ApexDriveRACKING
Featured Heavy-Duty Warehouse Storage Racking Systems
Engineered for maximum space efficiency, high throughput, and structural durability. Direct factory export with complete CE quality certifications.
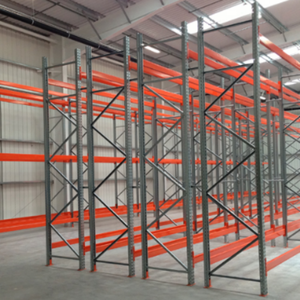
- Payload: 500 kg – 3,000 kg / level
- Access: FILO Double Deep System
- Material: Q235B Cold Rolled Steel
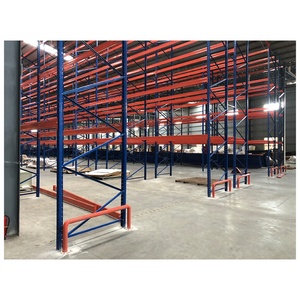
- Temp Range: Down to -30°C Cold Storage
- Coating: Epoxy Powder / Hot-Dip Galv
- Selectivity: 100% Direct Access
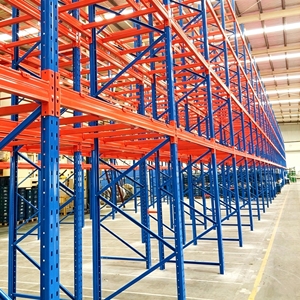
- Height Capability: Up to 12 meters
- Adjustability: 50mm / 75mm Pitch
- Safety: Structural Lock Pins Included
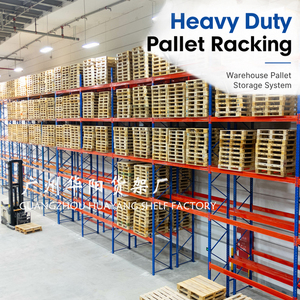
- Beam Load: Certified 3,000 kg/tier
- Standards: ISO 9001 & CE Compliant
- Frame Profile: Omega Upright Columns
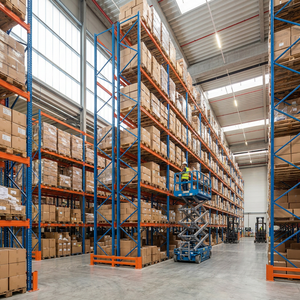
- Structure: Multi-tier Floor Compatible
- Options: Mesh / Steel / Wood Decking
- Finish: 180°C Cured Electrostatic
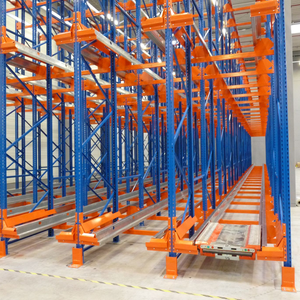
- Automation: Semi-Automated Shuttle Bot
- Mode: Switchable FIFO / LIFO
- Efficiency: +80% Density Boost
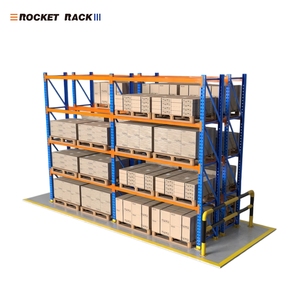
- Standard: FEM 10.2.02 / EN 15512
- Certification: Full CE Compliance Mark
- Tolerance: Cumulative Pitch ±2mm
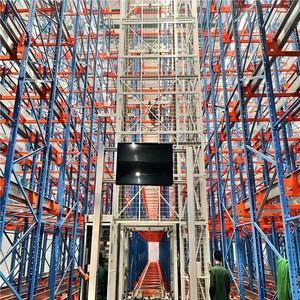
- Technology: 4-Directional Automated Rover
- Integration: WMS / WCS API Ready
- Utilization: Maximum Cube Density
Engineering Whitepaper: Maximizing High-Density Storage via Drive-Through Pallet Racking Systems
In modern supply chain management and intralogistics, warehouse spatial optimization and material handling efficiency dictate overall operational profitability. As a leading CE certified Drive-Through Pallet Racking Factory & Exporter, ApexDrive Industrial Racking Co., Ltd. delivers structural engineering solutions tailored for high-volume, high-density distribution centers. Drive-through racking—often evaluated alongside drive-in racking—represents a specialized continuous-lane structural configuration designed to optimize floor area utilization by up to 85% compared to standard selective pallet racking.
Unlike conventional selective racking which requires dedicated handling aisles for every two racking rows, drive-through systems eliminate work aisles entirely. Forklifts drive directly into the racking structure’s internal lanes to place or retrieve pallets supported on continuous cantilevered pallet rails. The defining operational advantage of a true Drive-Through layout is its dual-access architecture: forklifts can enter from the front entry face for loading and from the rear exit face for offloading. This enables genuine First-In, First-Out (FIFO) stock rotation, making it ideal for batch-manufactured goods, cold-chain food storage, pharmaceutical logistics, and fast-moving consumer goods (FMCG) with expiration constraints.
Technical Distinction: Drive-In vs. Drive-Through Racking
While Drive-In racking is closed at one end (forcing Last-In, First-Out / LIFO operation), Drive-Through racking remains open at both access points. This dual-access model requires strict structural cross-bracing engineering overhead at the top frame level (Top Tie Beams) to preserve structural integrity without blocking ground-level vehicle passages.
Structural Architecture and FEM 10.2.02 Engineering Standards
Because drive-through racking lacks standard horizontal support beams across the vehicle movement paths, all live loads are transferred to upright columns through cantilevered arm brackets and cold-formed pallet runner rails. This structural dynamic introduces significant horizontal sway potential and torsional moments during forklift positioning. Engineering a high-reliability drive-through system demands rigorous structural calculation under the European FEM 10.2.02 (Federation Europeenne de la Manutention) design code and EN 15512:2020 standards.
High-Tensile Prime Steel
Roll-formed strictly from certified Q235B and Q355B structural steel coils supplied by premier mills (Baosteel, Masteel). Yield strengths are verified up to 355 MPa to ensure minimal column buckling under static and dynamic loading.
Top Tie & Back Portal Frames
Heavy-duty top portal bracing beams integrate high-rigidity gusset plates. This top-level box frame distributes lateral sway forces evenly across adjacent lanes, guaranteeing vertical stability under M7 seismic ratings.
Floor-Anchored Guide Rails
To safeguard structural uprights against impacts from entering materials-handling equipment, floor-anchored steel ground rails (C-channel or heavy angle profiles) guide forklift tires down the entire lane length.
In-House Manufacturing Excellence & Surface Corrosion Defense
Quality control at ApexDrive Industrial Racking Co., Ltd. is enforced from raw material receipt through container loading. Component manufacturing occurs across our 20,000 m² modern facility using specialized automation tooling:
- Precision Cold Roll Forming: Uprights up to 12 meters in length are produced in single continuous profiles using continuous roll-forming lines. Cumulative hole-pitch location tolerance is maintained within ±2 mm over 12,000 mm, preventing beam tilt and uneven load distribution.
- Robotic MIG Welding: Bracket-to-arm and baseplate-to-column connections are executed using multi-axis robotic welding manipulators. This guarantees zero porosity, full penetration welds, and complete elimination of human error at critical load-bearing joints.
- 220-Meter Automated Powder Coating: All finished components undergo a 10-stage pretreatment process (degreasing, rust removal, zinc phosphate coating) followed by electrostatic powder deposition using Swiss Gema spray heads. The coating is cured at 180°C to achieve a durable, scratch-resistant finish exceeding 500 hours of salt-spray testing.
- Hot-Dip Galvanizing (Optional for Cold Chain): For sub-zero environments (-30°C) or highly humid processing facilities, structural components receive hot-dip galvanizing to BS EN ISO 1461 standards, offering 50+ years of rust prevention.
Comparative Engineering Matrix: Industrial Racking Options
Selecting the optimal racking system requires balancing spatial density against stock access flexibility. The data matrix below presents a structural and operational comparison across primary high-density storage formats:
| Storage System Type | Storage Density | Stock Access Rotation | Forklift Entry Required? | Floor Footprint Utilization | Best Industry Application |
|---|---|---|---|---|---|
| Drive-Through Racking | Very High (75-85%) | First-In, First-Out (FIFO) | Yes (Enters Rack Lane) | Up to 85% | Food & Beverage, Batch Mfg, Cold Storage |
| Drive-In Racking | Very High (75-85%) | Last-In, First-Out (LIFO) | Yes (Enters Rack Lane) | Up to 85% | Uniform SKUs, Non-perishable Bulk Goods |
| Selective Pallet Racking | Standard (40-50%) | 100% Direct Access | No (Aisle Operation) | 40-50% | High SKU Diversity, 3PL Fulfillment Hubs |
| Radio Shuttle Racking | Ultra High (85-90%) | Configurable (FIFO/LIFO) | No (Automated Bot) | Up to 90% | Deep Cold Chain, High Throughput Logistics |
| Four-Way AS/RS Shuttle | Maximum (90-95%) | Automated WMS Directed | No (Fully Automated) | Up to 95% | Smart Automated Warehouses, E-Commerce |
Future Procurement Trends: Drive-Through Racking Systems (2025–2030)
As global logistics operators navigate escalating real estate costs and supply chain volatility, procurement strategies for industrial storage equipment are evolving rapidly. Technical buyers and warehouse planners must align structural investments with several emerging trends:
1. Hybrid Integration with Autonomous Mobile Robots (AMRs) & AGVs
Traditional drive-through racking relied exclusively on human-operated reach trucks or counterbalance forklifts. Modern procurement specifications increasingly mandate AGV/AMR compatibility. This requires structural engineers to widen entry tolerances, integrate magnetic or laser positioning reflectors onto upright columns, and install heavy-duty ground-guided sensors. Drive-through lanes modified for AGVs eliminate human collision risks, delivering round-the-clock dark warehouse capabilities.
2. Stringent Seismic and Dynamic FEA Validation
With global building codes enforcing stricter safety margins in seismic zones, structural calculation reports based on Finite Element Analysis (FEA) are now mandatory for international tenders. Future-ready drive-through systems integrate high-ductility steel grades and specialized baseplate anchor assemblies that dissipate energy during seismic events, preventing progressive structural collapse.
3. Sustainability and Scope 3 Carbon Footprint Audits
Multinational buyers are evaluating racking manufacturers based on embodied carbon. Sourcing steel from green electric arc furnace (EAF) mills, utilizing low-VOC powder coatings, and optimizing loading container packing to minimize shipping emissions are becoming core criteria in international procurement RFQs.
Global Enterprise Advantages of Partnering with ApexDrive
As a premier China-based factory and global exporter with over 18 years of manufacturing experience, ApexDrive Industrial Racking Co., Ltd. delivers end-to-end service for high-capacity warehouse projects:
1. Free CAD & 3D Engineering
Our in-house structural engineering team provides complimentary CAD layout drawings, 3D renderings, and certified structural load reports tailored to your building height, floor slab load limits, and material handling fleet specs.
2. Factory Trial Assembly
Prior to international container shipping, critical components undergo trial shop-floor assembly to verify column alignment, hole-pitch accuracy, bracket fitment, and structural bolt hole positioning.
3. Export Packaging Protocols
Uprights and beams are bundled with multi-tier steel strapping and corner edge protectors. Hardware fasteners, safety pins, and baseplates are packed in export-grade plywood crates to ensure zero damage during ocean transit.
Frequently Asked Questions (FAQ) for Technical Buyers & Importers
What parameters are required for ApexDrive to generate a free layout design?
To prepare an accurate engineering drawing and structural quote, we require: (1) Building architectural CAD drawings or dimensions showing clear height, column grid locations, and door locations; (2) Pallet dimensions including load height and total weight per pallet load; (3) Operational rotation requirements (FIFO or LIFO); and (4) Forklift specifications including maximum lift height and minimum right-angle stacking aisle width.
How does CE certification benefit international racking importers?
CE certification verifies that our drive-through and selective pallet racking systems comply with mandatory European safety, health, and environmental protection requirements (under EN 15512 and FEM standard guidelines). For importers and project owners, this streamlines customs clearance, lowers facility insurance premiums, and ensures compliance with local workplace safety audits.
Can drive-through racking withstand cold storage conditions down to -30°C?
Yes. We manufacture cold-storage dedicated racking using low-temperature impact-resistant steel grades (such as Q355D/E) treated with specialized cold-room powder coating formulations or hot-dip galvanizing. This prevents hydrogen embrittlement of steel welds and coating flaking under freeze-thaw cycles.
What installation support is provided for overseas projects?
Every export shipment includes comprehensive English assembly manuals, structural layout key plans, and step-by-step installation videos. Our engineering team provides real-time online video guidance during assembly. For large distribution centers, ApexDrive can dispatch certified installation supervisors directly to your project site.
What safety accessories are recommended for drive-through racking lanes?
Because forklifts maneuver inside the racking lanes, we strongly advise installing: (1) Heavy-duty floor guide rails to keep vehicles centered; (2) Column upright protectors at entry faces; (3) Pallet backstops to prevent over-pushing; and (4) High-visibility yellow powder coating on lane entry frames.
Request a Free Engineering Layout & Factory Quotation
Contact our senior structural engineers today. Receive your CAD design, certified load capacities, and direct factory pricing within 24 hours.