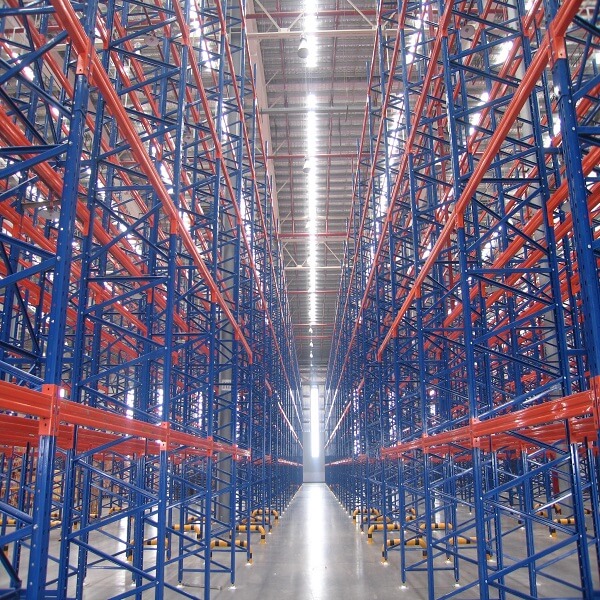
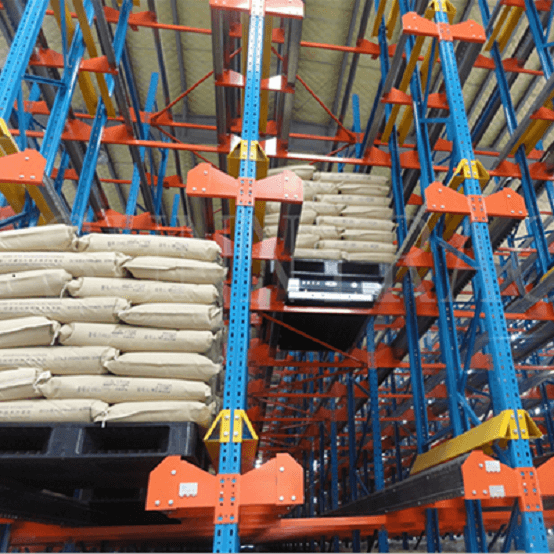
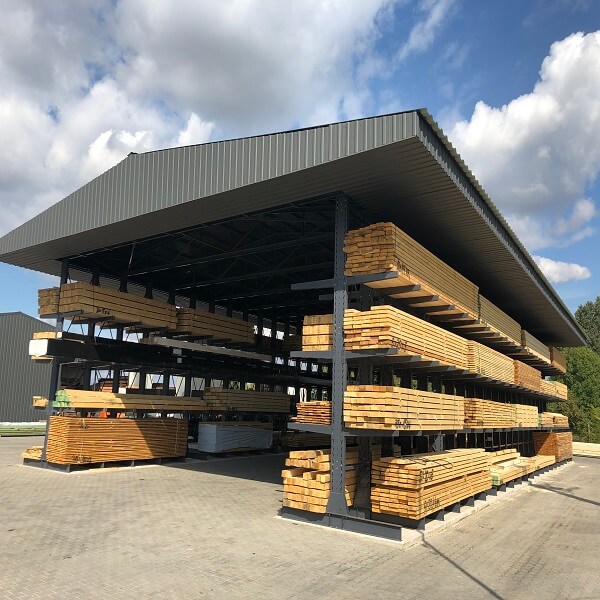
High-density Electric Mobile Racking System installed in industrial logistics warehouse by ApexDrive Industrial Racking Co., Ltd.
High-Density Motorized Storage Engineering

Electric Mobile Racking System: Double Storage Density, Zero Wasted Aisles

  • Up to 85% Increase in Storage Capacity
  • 100% Direct SKU Selectivity with Single-Aisle Automation
  • Q235B / Q355B Steel Built for Heavy Loads & Cold Storage
Cold storage Electric Mobile Racking System layout engineering
Cold Chain & Energy Savings

Engineered for Cold Storage Efficiency & Sub-Zero Performance

  • Operates flawlessly down to -30°C
  • Cuts refrigerated footprint by up to 50%
  • PLC & WMS Controlled Soft-Start Motion Control
Heavy duty motorized mobile racking chassis and rail infrastructure
Triple-Layer Safety Protection

Fail-Safe Industrial Automation for Personnel & Goods

  • Photoelectric infrared barrier sensors
  • Emergency touch bars & optical distance locks
  • ISO 9001:2015 & CE Certified structural integrity
CECE CertifiedMobile Racking System
ISOISO 9001:2015Verified Quality
0%

Storage Density Increase

0%

Warehouse Footprint Reduction

0t+

Annual Production Capacity

0+

Global Installations Completed

Executive Engineering Overview

The Definitive Guide to Electric Mobile Racking Systems: Engineering, ROI & Global Procurement Trends

As industrial land costs soar and cold storage energy demands surge worldwide, procurement directors, supply chain VPs, and logistics engineers face a critical challenge: How do you double storage capacity without expanding your physical warehouse footprint?

The Electric Mobile Racking System (also referred to as Motorized Mobile Pallet Racking or Mobile Rack Systems) has emerged as the global benchmark for high-density, 100% selective pallet storage. By mounting conventional heavy-duty selective pallet racks or cantilever frames onto electronically driven mobile bases (carriages) that travel along floor-embedded steel rails, an Electric Mobile Racking System eliminates dedicated static operating aisles. Instead, a single operational aisle opens on demand via RF remote control, PLC interface touchscreens, or automated Warehouse Management Systems (WMS).

At ApexDrive Industrial Racking Co., Ltd., we bring over 18 years of specialized structural racking design, roll-forming precision, and automation integration to global buyers. From pharmaceutical clean-room cold vaults in Europe to heavy manufacturing distribution centers across North and South America, our engineered Electric Mobile Racking Systems deliver maximum cubic efficiency, operational safety, and unbeatable long-term ROI.

Engineering Quality & Precision

Technical Specifications & Structural Architecture

Safety, stability, and durability are non-negotiable when moving thousands of tons of dynamic steel loads. Here is how ApexDrive Industrial Racking Co., Ltd. engineers enterprise-grade reliability.

Certified Raw Materials

Mill-Traceable Steel
  • Q235B & Q355B structural steel from Baosteel & Masteel
  • Structural safety factor of 1.8 for upright design
  • Complete mill certificates supplied with every project batch

Precision Drive Mechanics

Synchronized Motion Control
  • Multi-wheel heavy-duty cast steel chassis with dual-drive shafts
  • Variable Frequency Drives (VFD) for soft start and smooth stop
  • Siemens PLC & Schneider electrical control modules

Triple Safety Architecture

Fail-Safe Operation
  • Full-height photoelectric sensor curtains across moving aisles
  • Physical emergency stop bumpers along bottom chassis rails
  • Visual strobe warnings and audible alarms during rack transit

Precision Rail Systems

Smooth Carriage Transit
  • High-grade surface-mounted or floor-embedded steel rails
  • Levelling tolerances engineered strictly within DIN 15185
  • Anti-seismic guide profiles to prevent rack tilt during movement

Advanced Surface Protection

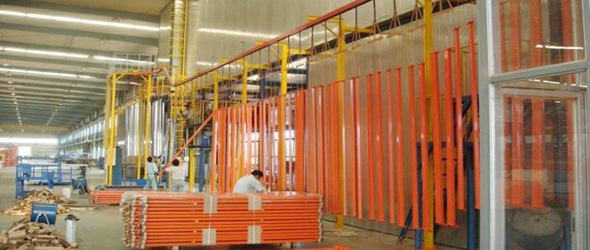
220m Automated Powder Line
  • 10-stage automatic degreasing and surface pretreatment
  • Swiss Gema electrostatic powder spraying equipment
  • 180°C thermostatic curing for scratch and rust resistance

Smart System Integration

WMS & AGV/AMR Ready
  • RF remote controllers for forklift operators
  • Profinet / Ethernet connection for automatic WMS aisle opening
  • Night-spacing / ventilation mode for optimized cold airflow
Decision Matrix

Warehouse Storage Systems Technical & Financial Comparison

Evaluating high-density storage technologies? Compare how an Electric Mobile Racking System measures up against conventional pallet rack, Radio Shuttle, and AS/RS systems.

Comparison based on standardized 10,000-pallet warehouse footprint and operational parameters.
Storage System Floor Space Utilization Direct SKU Access Cold Storage Energy Efficiency Initial Capex Investment Forklift Fleet Requirement
Electric Mobile Racking (Up to 85%) 100% Direct Selectivity Excellent (Reduces cooled volume 45%) Moderate – High ROI Standard Forklifts
Selective Pallet Racking (Baseline 40%) 100% Direct Selectivity Poor (Wastes footprint on static aisles) Low Standard Forklifts
Radio Shuttle Racking (Up to 75%) LIFO / Batch FIFO only Very Good Moderate Forklift + Shuttle Unit
Automated Storage & Retrieval (AS/RS) (Up to 90%) 100% Automated Selectivity Maximum Efficiency Very High Automated Stacker Crane
Why Choose Us

Manufacturing Excellence at ApexDrive Industrial Racking Co., Ltd.

Over 18 years of manufacturing expertise, 20,000+ m² production facilities, and rigorous ISO 9001 quality management ensure your warehouse project is executed flawlessly.

Factory-Direct Scale

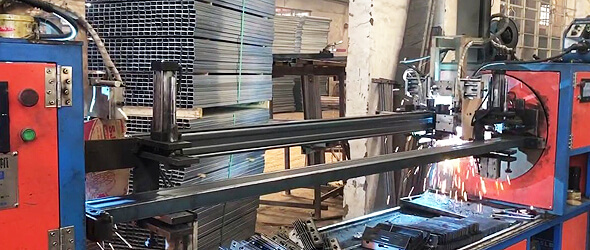
20,000 m² factory area with over 150 sets of advanced metal-forming and welding equipment yielding 30,000+ tons of annual output.

Precision Roll Forming

German-technology automatic continuous roll-forming lines maintain a cumulative hole-pitch tolerance within ±2 mm over 12 meters.

220m Powder Line

Swiss Gema coating systems deliver superior paint adhesion, uniform coating thickness, and robust corrosion resistance.

100% Pre-Assembly QC

Every Electric Mobile Racking chassis and electrical panel undergoes trial assembly and movement testing prior to export packing.

Factory Production Quality

End-to-End Manufacturing Control for Mobile Racking Systems

Every component of an Electric Mobile Racking System undergoes six strict manufacturing phases inside our Nanjing production complex.

Steel raw material inspection for Electric Mobile Racking manufacturing
01

Raw Materials — High Yield Q355B Steel

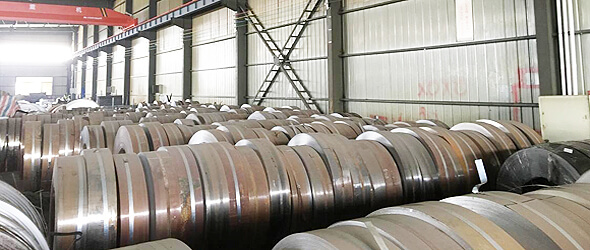
We source prime steel coils exclusively from Tier-1 mills (Baosteel, Masteel, Shougang). Steel thickness, yield strength, and chemical composition are verified against mill certificate standards prior to production.

  • Q235B / Q355B Grade
  • Mill Test Reports
  • Strict QC
German-technology continuous roll forming machine for mobile racking columns
02

Roll Forming — ±2 mm Over 12 m Lengths

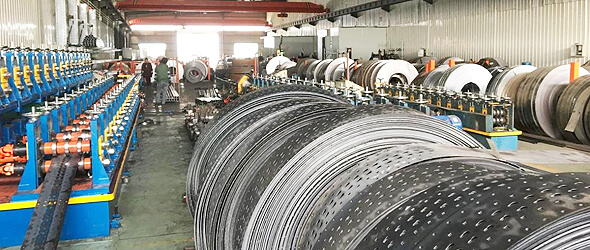
Uprights and mobile base beam profiles are cold roll-formed on automated precision lines. Accurate hole punching ensures seamless bolting during field installation overseas.

  • German Technology
  • 12m One-Piece Upright
  • High Precision
Robotic welding manipulator fabricating heavy duty mobile chassis
03

Welding — Robotic Manipulators

Heavy mobile carriage wheel housings and load-bearing beam connectors are welded using automatic robotic manipulators, eliminating manual defects, missed seams, and stress concentrations.

  • Robotic Accuracy
  • Full Penetration
  • Zero Defect
220m automatic powder coating line for racking surface treatment
04

Surface Coating — 220m Automatic Line

Parts undergo multi-stage chemical degreasing, rust removal, and phosphate washing before entering our 220-meter automated electrostatic powder line equipped with Swiss Gema guns.

  • Swiss Gema Spraying
  • 180°C Curing
  • Durable Finish
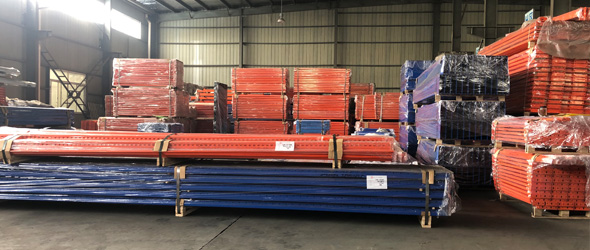
Export steel strapping and pallet packing for global mobile racking shipments
05

Export Packaging — Zero Transit Damage

Racking uprights and mobile chassis beams are bundled with steel strapping and protective edge covers. Electrical control panels, gear motors, and sensors are boxed in sealed plywood crates.

  • Plywood Crates
  • Heavy Steel Strapping
  • Customs Labeled
Turnkey Execution

ApexDrive Engineering & Project Process

From architectural floor assessment to on-site commissioning, ApexDrive Industrial Racking Co., Ltd. provides a single point of accountability.

  1. Consultation icon01

    Requirements Inquiry

    Engineers analyze pallet specs, SKU throughput, floor load limits, and ceiling heights.

  2. Survey icon02

    Floor & Site Survey

    Detailed evaluation of slab concrete strength, rebar placement, and levelling specs.

  3. CAD Design icon03

    3D CAD Layout

    Free engineering design, structural stress calculations, and motor power requirements.

  4. Optimization icon04

    Optimization

    Refining mobile block zoning, aisle opening speed, and electrical control architecture.

  5. Contract icon05

    Contract & Specs

    Finalizing steel grades, motor brands (Siemens/SEW), timeline, and warranty terms.

  6. Production icon06

    In-House Production

    Precision roll-forming, robotic welding, powder coating, and pre-assembly testing.

  7. Installation icon07

    Overseas Installation

    Complete CAD drawings, English manuals, online video guidance or engineer dispatch.

  8. After-Sales icon08

    After-Sales Support

    Lifetime technical support, spare parts supply, and remote PLC diagnostic support.

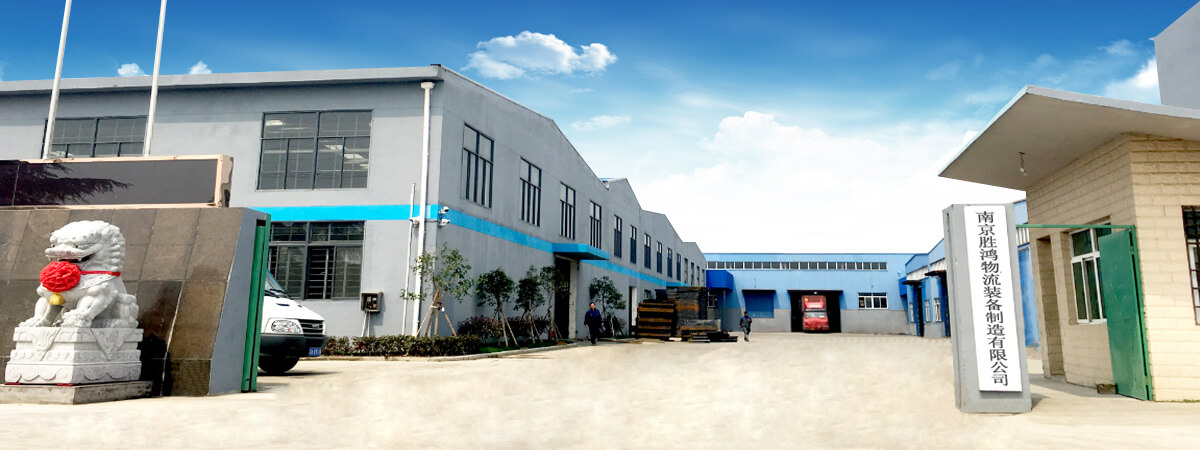
ApexDrive Industrial Racking Co., Ltd. headquarters and manufacturing factory
2006Founded in Nanjing, China
Company Credibility

ApexDrive Industrial Racking Co., Ltd. — Your Trusted Storage Racking Partner

Established in September 2006, ApexDrive Industrial Racking Co., Ltd. is a premier Chinese manufacturer specializing in high-density warehouse racking and logistics automation systems. Operating from a modern 20,000 m² manufacturing facility in Nanjing, we engineer, fabricate, and deliver custom structural solutions for clients in over 60 countries.

Our comprehensive portfolio includes Electric Mobile Racking Systems, Selective Pallet Racking, Radio Shuttle Racking, Multi-Tier Mezzanine Racking, Heavy-Duty Cantilever Racking, Industrial Steel Platforms, and Automated Storage & Retrieval Systems (AS/RS). Every system complies strictly with FEM 10.2.07, RMI, and EN safety standards.

  • Free layout & engineering design
  • 100% Trial assembly before shipping
  • ISO 9001:2015 & CE Certified
  • Global installation & remote support
Inquire Now

International Quality Certifications

Independent third-party verification confirming full compliance with global manufacturing and safety norms.

Buyer Knowledge Base

Frequently Asked Questions on Electric Mobile Racking Systems

Comprehensive answers compiled by our senior structural engineers to address common questions raised by international procurement managers and warehouse operators.

What is an Electric Mobile Racking System and how does it save warehouse space?
An Electric Mobile Racking System consists of heavy-duty selective pallet racks or cantilever racks mounted onto motorized mobile carriages that move along steel rails embedded in the floor. By consolidating multiple static aisles into a single operational aisle that opens electronically on demand, the system eliminates up to 85% of wasted aisle space, effectively doubling your available pallet storage within the same facility footprint.
What concrete floor requirements are needed to install an Electric Mobile Racking System?
Because high-density point loads are transferred through the mobile carriage wheels into the floor rails, the concrete slab must meet specific structural requirements: a minimum thickness of 200 mm to 250 mm with C30/C35 grade reinforced concrete, and floor flatness tolerances adhering to DIN 15185 or VDMA standards. ApexDrive Industrial Racking Co., Ltd. provides complete concrete slab loading specs and rail embedding drawings before installation.
How does the safety system protect operators and forklifts inside an open aisle?
Our Electric Mobile Racking Systems incorporate a multi-tiered fail-safe safety architecture: (1) Full-height photoelectric light curtains positioned at the aisle entry points that instantly halt movement if a person or forklift enters; (2) Mechanical pressure-sensitive emergency stop bars running along the bottom chassis; (3) Optical distance sensors preventing carriage-to-carriage collisions; and (4) Visual strobe lights with acoustic warning signals active during movement.
Can an Electric Mobile Racking System operate reliably in cold storage (-30°C)?
Yes. ApexDrive Industrial Racking Co., Ltd. custom engineers cold-storage versions rated down to -30°C. These systems feature specialized low-temperature lubricants, internal heating elements for PLC control cabinets, IP65 water/ice-resistant electrical enclosures, and cold-treated steel components. Furthermore, mobile racking reduces cold room volume by up to 50%, cutting refrigeration electrical costs significantly.
What happens during a power outage? Can goods still be accessed?
In the event of a power failure, our control systems can be powered by an auxiliary diesel generator or an Uninterruptible Power Supply (UPS) backup module to open essential aisles. Additionally, every mobile carriage features a manual brake release mechanism, allowing emergency manual movement of carriages using a hand crank if complete electrical loss occurs.
How does an Electric Mobile Racking System integrate with WMS or AGVs?
Our PLC control units support standard industrial communication protocols (Ethernet/IP, Profinet, Modbus). When integrated with a Warehouse Management System (WMS) or AGV fleet management software, the WMS automatically commands the target mobile aisle to open as an AGV or forklift approaches the rack block, optimizing picking sequences and reducing travel time.
What is the typical maintenance schedule for motorized mobile carriages?
Routine maintenance is straightforward: monthly visual inspections of optical light curtains and floor rail grooves; quarterly checks of drive chain tension, wheel gear lubrication, and electrical terminals; and annual inspections of motor gearboxes and structural bolt tightness. ApexDrive Industrial Racking Co., Ltd. supplies a comprehensive maintenance checklist and spare parts kit with every export project.
How does ApexDrive Industrial Racking Co., Ltd. support installation for overseas orders?
We provide complete installation support for global projects: comprehensive 3D CAD assembly drawings, step-by-step English installation manuals, and wiring schematics. Our technical team conducts video conferences during assembly, and for complex or high-bay installations, senior engineers can be dispatched to your facility to oversee installation and commissioning.