Engineered High-Density Motorized Racking for Modern Warehouses
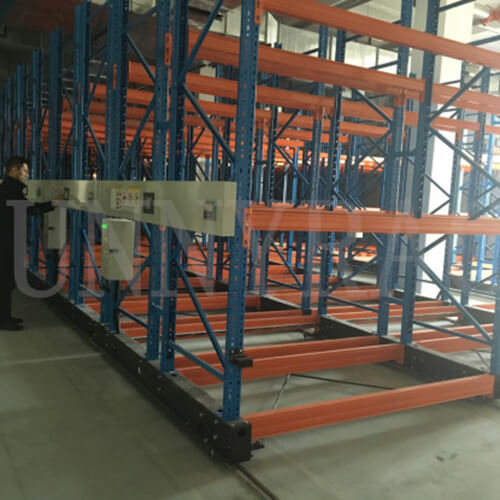
The Electric Mobile Racking System manufactured by ApexDrive Industrial Racking Co., Ltd. is a high-density, motorized storage solution designed for commercial warehouses where footprint cost is critical. By mounting conventional pallet racking blocks onto heavy-duty electronically driven mobile bases guided by floor-embedded tracks, multiple static access aisles are compressed into a single dynamic operational aisle.
When an operator commands an aisle via remote control, central touch-screen PLC, or integrated WMS, motorized carriages glide smoothly across floor rails to create a wide forklift access aisle directly at the target rack bay. This architecture provides up to 80% to 90% floor area utilization while ensuring 100% individual selectivity to every SKU, making it an exceptional investment for cold storage facilities, raw materials storage, and high-value industrial goods.
Key Engineering Advantages
Doubled Storage Capacity
Eliminating static corridors and maintaining only one working aisle compresses rack volume, doubling storage density compared with traditional selective pallet racking within the identical building footprint.
Substantial Energy Savings
Widely deployed in cold chains and freezers down to -30°C. Dramatically reducing cubic air volume per stored pallet slashes refrigeration, lighting, and HVAC utility costs per pallet location.
100% Pallet Accessibility
Unlike drive-in or push-back systems that enforce strict batch LIFO/FIFO patterns, electric mobile bases can expose any individual pallet bay in seconds, maintaining complete direct-access picking flexibility.
Multi-Tier Safety Architecture
Equipped with dual photoelectric anti-collision safety barriers, perimeter emergency stop bars, laser distance sensors, and automated safety interlocks complying strictly with CE industrial safety standards.
Technical Specifications
| Structural Steel Grade | Certified Q235B & Q355B cold roll-formed structural steel from prime mills |
|---|---|
| Carriage Load Capacity | Up to 24–32 tons per mobile base carriage (custom engineered per project) |
| Drive & Motor System | Multi-wheel synchronized motorized transmission, IP54/IP65 geared motors with soft-start & soft-stop control |
| Control Architecture | Siemens PLC controller, touch screen HMI, hand-held wireless RF remote, optional WMS interface |
| Travel Speed | 4.5 to 6.0 meters per minute (optimized for smooth movement and cargo stability) |
| Operating Temperature | Standard ambient (-5°C to +40°C) or specialized low-temperature cold store configuration (-30°C to +5°C) |
| Floor Rail Requirements | Precision leveling embedded guide rails and flat load-bearing rails flush with the warehouse floor surface |
| Surface Finish | Degreased, phosphate rust-inhibited, electrostatic powder-coated at 180°C (Hot-dip galvanizing available) |
System Operational Modes
Forklift operators activate the required bay remotely from the cabin via radio frequency transmitters, opening the target aisle before arrival.
At shifts end or in cold storage facilities, carriages automatically space evenly to facilitate air circulation, cooling efficiency, and fire system compliance.
In routine maintenance or power-outage contingencies, carriages can be operated via localized manual override panels or emergency power packs.
Request a Custom Electric Mobile Racking Layout
Our senior warehouse engineers provide free CAD layout design, floor rail engineering diagrams, and load calculation reports tailored to your building clear height and SKU requirements.