ApexDriveRACKING
Product Catalog
Engineered Industrial Storage Systems
Explore our CE-certified gravity roller racks, selective pallet frames, and heavy-duty logistics structures.
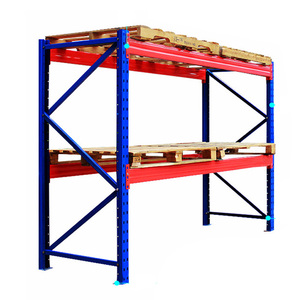
Outdoor Pallet Racking Metal Storage Organizer Rack For Warehouse Store Factory 1000KG 2000KG 3000KG Pounds Tons
Contact Us
Prefabricated Steel Structure Logistics Warehouse Workshop Industrial Building Commercial Building Steel Structure Warehouse
Contact Us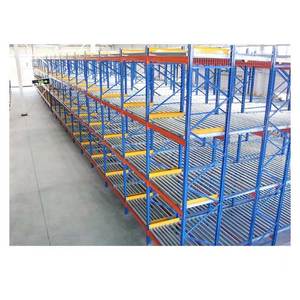
CE Certified Anti-Rust 2000kg Load Capacity Gravity Pallet Racking High Quality Heavy Duty Roller Pallet Rack
Contact Us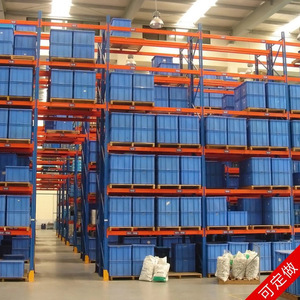
Heavy Duty Cold Rolled Steel Multi-Layer Pallet Racking High Bay Warehouse Storage System Epoxy Powder Coated Construction
Contact Us
Warehouse Heavy Duty Industrial Shelves Steel EU Blue and Orange Selective Pallet Racking Shelving System CE Certified
Contact Us
Manufacturer Pallet Shelf Systems European Standard Warehouse Squat Rack Racks for Factory
Contact Us
Blue Orange Customizable Colors Industrial Stacking Racks Heavy Duty Steel Pallet Rack System Warehouse Storage Shuttle Racking
Contact Us
Warehouse Shelving Heavy Duty Shelves Multi Level Pallet Rack Factory Industrial Racking Systems
Contact Us20,000+ m²
Production Facility
30,000 Tons
Annual Steel Output
6,000+
Global Projects Installed
CE & ISO
Certified Compliance
Executive Overview: Engineering Excellence in Pallet Flow Racking
Pallet Flow Racking—commonly referred to as Gravity Flow Racking or live pallet storage—represents the pinnacle of dynamic, high-density, First-In, First-Out (FIFO) warehouse engineering. Operating purely on gravitational kinetic energy, pallet flow systems eliminate internal forklift travel aisles by utilizing inclined roller tracks set at precise pitch gradients (typically 3.5% to 4.5%). As loaded pallets are placed at the high-end loading aisle, gravity gently drives them forward toward the discharge picking interface at a controlled terminal velocity.
As a leading CE Certified Pallet Flow Racking Supplier & Suppliers network, our manufacturing standard mandates structural integrity, zero power consumption logistics, and failure-proof mechanical speed regulation. In modern cold-chain operations, fast-moving consumer goods (FMCG) logistics, and pharmaceutical distribution hubs, gravity live racking provides up to 60% higher floor space utilization compared to conventional selective pallet racking systems while securing strict batch rotation.
Key Kinematic Components of Heavy-Duty Gravity Roller Racks
Precision-Graded Roller Tracks
Cold-rolled steel or high-impact poly-wheels equipped with dual-shielded ball bearings. Designed to withstand point loads from 1000kg to 3000kg per pallet position without permanent deformation.
Indirect Dynamic Speed Controllers
Magnetic or centrifugal braking rollers strategically inserted along the lane pitch to limit pallet velocity to a safe operating speed of 0.25 m/s to 0.30 m/s regardless of pallet load weight.
Safety Separator Mechanisms
Engineered mechanical stop-and-release separators that isolate the lead pallet at the picking front from line pressure behind it, ensuring stress-free forklift extraction without binding.
CE Certification & Structural Compliance Standards
When selecting a pallet flow racking supplier, European conformity (CE Marking) is not merely a label—it is a rigorous proof of mechanical structural safety under finite element analysis (FEA) and dynamic stress testing. Our pallet flow systems strictly comply with European Standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design) and FEM 10.2.02 standards.
Raw steel coils are procured directly from certified tier-1 steel mills including Baosteel, Masteel, and Wuhan Iron and Steel. Components are roll-formed using structural grade Q235B and Q355B high-yield strength steel, guaranteeing superior elasticity, dynamic load carrying capacity, and cold resistance down to -30°C in refrigerated storage facilities.
Technical Specification & System Performance Matrix
| System Parameters | Pallet Flow Racking (Live FIFO) | Selective Pallet Racking | Radio Shuttle Racking | Drive-In Racking |
|---|---|---|---|---|
| Storage Density Efficiency | Extremely High (Up to 85%) | Moderate (approx. 40%) | Very High (Up to 80%) | High (approx. 65%) |
| Stock Rotation Principle | Strict FIFO (First-In, First-Out) | 100% Random Access | FIFO / LIFO Optional | Strict LIFO (Last-In, First-Out) |
| Operative Energy Consumption | 0 kWh (Pure Gravity Kinetic) | 0 kWh (Manual Forklift) | Battery Electric Shuttle | 0 kWh (Manual Forklift) |
| Forklift Travel Inside Lanes | None (Aisle-Bound Only) | Requires Aisle per Row | None (Aisle-Bound Only) | Deep Rack Entry (High Risk) |
| Pallet Weight Range | 1000 KG to 3000 KG / Pallet | 500 KG to 4000 KG / Tier | 500 KG to 1500 KG / Pallet | 500 KG to 1500 KG / Pallet |
| CE & EN Standard Compliance | EN 15512 / FEM 10.2.02 | EN 15512 / ISO 9001 | CE Machinery Directive | EN 15512 Compliance |
Future Procurement Trends in Heavy-Duty Pallet Flow Racking
As global supply chains shift toward rapid order fulfillment, omni-channel e-commerce, and automated cold-chain logistics, global warehouse procurement directors are reframing their capital investment criteria. Key macro trends shaping the procurement of pallet flow systems include:
1
Hybrid Automation Integration
Future pallet flow racking systems are increasingly configured to interface directly with Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs) at both loading and picking interfaces, eliminating manual forklift operations entirely.
2
IoT-Monitored Smart Braking Rollers
Sensors embedded within magnetic speed controllers provide real-time vibration, temperature, and impact analytics, allowing predictive maintenance alerts before roller failure or lane jamming occurs.
3
Zero-VOC Electrostatic Powder Coating
Environmental regulations require ultra-durable, non-gassing thermosetting powder coatings cured at 180°C. Our 220-meter automated surface line delivers anti-corrosive, scratch-resistant powder coatings tailored for strict hygiene and food safety environments.
4
Modular Field Reconfigurability
Procurement teams demand system modularity. Modern roller lanes feature clip-in track supports, variable roller pitch increments (50mm / 75mm / 100mm), and adjustable slope brackets to handle shifting pallet quality standards (e.g., Euro pallets vs. GMA pallets).
Next-Generation Technological Innovations in Live Gravity Racking
Overcoming system friction, structural deflection, and pallet runaway risks has historically required high-end precision engineering. Our R&D team has pioneered several breakthrough technological refinements in gravity rack production:
1. Magnetic Non-Contact Speed Regulation: Traditional friction-based brake rollers suffer from rubber wear and thermal degradation during high-frequency cycles. Next-generation magnetic braking controllers utilize eddy-current resistance. The faster a pallet rolls, the greater the counter-retardation force applied without mechanical surface contact, yielding zero friction wear and a extended service life exceeding 10 years.
2. Progressive Safety Separator Springs: Traditional mechanical separators rely on simple counterweights or basic tension springs that fail after tens of thousands of cycles. Our patented progressive separation latch system features heavy-duty alloy torsion springs capable of surviving 500,000 actuation cycles, completely shielding forklift operators from the hydrostatic forward thrust of backlogged pallets.
3. Anti-Crush Pallet Entry Guides: Entry funnel guides formed from high-density polyethylene (HDPE) combined with tapered steel profiles prevent damaged wooden pallets from misaligning or derailing upon insertion at high elevation bays.
Factory Strength & Comprehensive Manufacturing Capabilities
Partnering directly with a tier-1 CE Certified Pallet Flow Racking Manufacturer & Supplier gives global importers, warehouse integrators, and industrial end-users an undeniable cost and quality advantage. Our state-of-the-art manufacturing infrastructure in Nanjing, Jiangsu includes:
20,000+ m² Production Hub
Equipped with 150+ sets of advanced manufacturing machinery including German roll-forming lines, automated punch presses, laser cutting cells, and robotic welding manipulators.
Full Process Quality Assurance
From chemical analysis of raw Q235B/Q355B coil steel to ultrasonic weld testing, 100% pre-shipment trial assembly, and 8.8-grade structural bolt torque checks.
220m Automatic Powder Coating Line
Multi-stage chemical degreasing, surface de-rusting, zinc phosphate pre-treatment, electrostatic powder deposition, and 180°C high-temperature curing for total anti-corrosion protection.
Frequently Asked Procurement & Engineering Questions (FAQ)
Q1: How do engineers calculate the precise slope gradient for Pallet Flow Racking?
The standard incline angle for pallet flow lanes ranges between 3.5% and 4.5% (approx. 3.5 cm to 4.5 cm drop per linear meter). The exact slope is determined based on pallet quality (wooden, plastic, steel), bottom runner orientation, total load weight (ranging from 500kg up to 3000kg), and warehouse operating ambient temperature (ambient vs cold storage). Our engineers perform physical slope flow testing prior to final production.
Q2: What pallet specifications are required for reliable gravity flow operation?
Pallet condition is critical in live flow systems. Pallets must feature intact bottom runner boards free from broken slats, protruding nails, or severe sag deflection (deflection ratio must not exceed L/300). Standard Euro pallets (800x1200mm), Industrial pallets (1000x1200mm), and customized GMA wooden or heavy plastic pallets with flat bottom runners work reliably.
Q3: How does your pallet flow racking system handle cold storage environments down to -30°C?
Cold storage setups feature specialized low-temperature synthetic lubricants inside the roller ball bearings, stainless steel roller shafts, and low-temp resilient brake controller seals. Furthermore, structural frames utilize Q355B cold-rolled steel tested for high impact toughness at sub-zero temperatures to prevent brittle fracture.
Q4: Why is a Safety Separator required at the discharge interface?
In deep pallet flow lanes (e.g., 5 to 20 pallets deep), the combined weight of accumulated pallets creates immense line pressure (back pressure) against the lead pallet at the picking face. Without a safety separator, a forklift cannot safely lift and extract the lead pallet without dangerous binding or rubbing against the second pallet. The separator holds back the trailing pallets until the lead pallet is completely removed.
Q5: What certifications and quality documentation accompany export shipments?
Every order shipped internationally includes complete material mill certificates, ISO 9001:2015 quality compliance reports, CE Conformity Declarations for European import validation, factory load testing certificates, 3D CAD assembly drawings, and comprehensive English installation manuals.
Optimize Your Warehouse Floor Space with CE Certified Pallet Flow Solutions
Consult with our senior structural storage engineers today for a free warehouse CAD layout design, static structural calculations, and competitive factory-direct pricing.
Contact Us