ApexDriveRACKING
20,000+ m²
Production Base
30,000+ Tons
Annual Capacity
CE & ISO 9001
Global Compliance
6,000+
Global Projects Delivered
Certified Pharmaceutical Storage Racking Solutions
Engineered to withstand rigorous cleanroom sanitization, cold-store environments (-40°C), and high-bay automation loads.
CE Certified
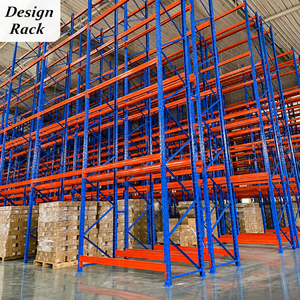
Certificated Large Heavy Duty Shelving Storage Applications Easy Assemble Material Racking Unit Industrial Pallet Rack Solution
Corrosion Protected
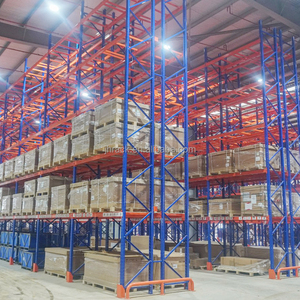
Heavy-Duty Corrosion Protected Pallet Racking Systems For Warehouse And Factory Storage By Jinhui Warehousing Suppliers
High Selectivity
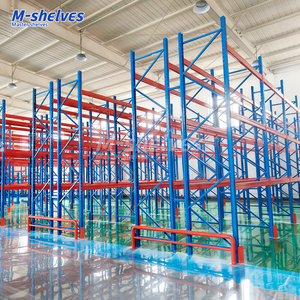
Warehouse Shelves Pallet Racking System Storage Heavy Duty Shelving Rack Pallet Racking Warehouse Racks
OEM/ODM Custom
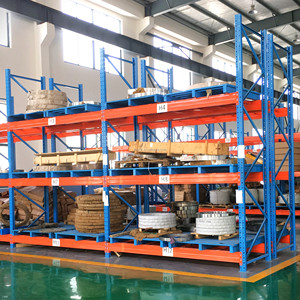
OEM Factory Wholesale Warehouse Racking Industrial Racks Customized Pallet Racking System Heavy Duty Steel Racks For Storage
Up to 3000kg/Layer
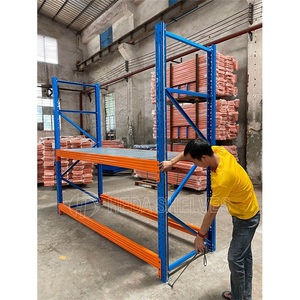
Mracking Heavy Duty Metal Pallet Storage Racking 1000kg/2000kg/3000kg Per Layer Industrial Pallet Shelving Rack
High Density
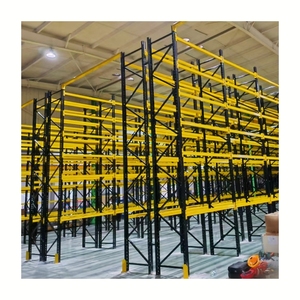
Customized Colors Storage Shelf High Density Pallet Racking Warehouse Racks Steel Heavy Duty Shelving For Warehousing
Coldroom Drive-In
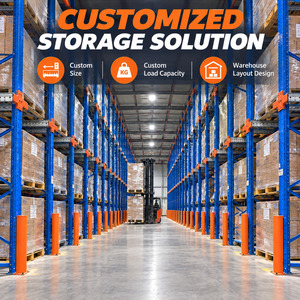
ODM OEM Q235 Steel Heavy Duty High Density Coldroom Coldstore Drive-in Through Pallet Racking Warehouse Storage System
Euro Standard
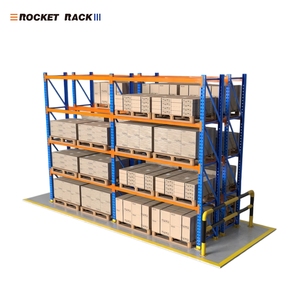
ROCKET RACK Europe Standard Industrial Racks CE Certified Heavy Duty Pallet Racking System for Warehouse Storage
Pharmaceutical Logistics Infrastructure: Engineering for GDP & GMP Integrity
In global pharmaceutical logistics, storage infrastructure is far more than simple structural steel. Modern cold-chain supply chains, biological manufacturing hubs, and active pharmaceutical ingredient (API) distribution networks demand storage racking systems engineered to strict International Good Distribution Practice (GDP) and Good Manufacturing Practice (GMP) protocols. Storage failure, thermal bridging, structural sagging, or microscopic paint flaking can lead to batch contamination, regulatory compliance failure, and multi-million-dollar inventory loss.
As a premier CE Certified Pharmaceutical Pallet Racking Supplier & Exporter, ApexDrive Racking delivers heavy-duty pallet racking systems designed around structural integrity, anti-corrosion science, and spatial precision. Utilizing structural Q235B and Q355B prime steel sourced directly from Tier-1 mills (Baosteel, Masteel, Wuhan Iron & Steel), our racking systems maintain absolute stability under heavy static loads, dynamic forklift impacts, and seismic forces up to M7 magnitude.
Information Gain Benchmark: Unlike standard commercial storage racks, pharmaceutical racking requires non-toxic, anti-bacterial electrostatic powder coatings cured at 180°C to guarantee zero chemical off-gassing, resistance to aggressive chemical disinfectants (peracetic acid, isopropyl alcohol), and zero structural deflection exceeding L/300 under maximum load.
Every racking component—from roll-formed upright profiles to robotic welded beam connectors—is produced on automated German-technology lines. Cumulative hole-pitch tolerances are constrained to within ±2 mm over a 12-meter upright length. This ultra-high mechanical precision guarantees even load redistribution across beam levels, preventing localized metal fatigue and ensuring seamless integration with Automated Storage and Retrieval Systems (AS/RS) and automated guided vehicles (AGVs).
Engineering Specifications & Structural Comparison Matrix
Selecting the appropriate pallet racking configuration depends on SKU density, turnover frequency, picking methodology, and cleanroom or cold-store environmental constraints. Below is an engineering overview of our core pharmaceutical racking architectures:
| Racking System Type | Material Grade | Storage Density | Stock Flow Rule | Temperature Range | Primary Pharma Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B Steel | Standard (100% Access) | FIFO (First-In, First-Out) | -20°C to +50°C | Multi-SKU Finished Products, Batch QC Quarantine |
| Radio Shuttle Racking | Q355B Cold-Formed Steel | Ultra-High (Deep Lane) | FIFO / LIFO Configurable | -30°C to +40°C | Cold Storage Vaccines, Biologics, Bulk Packaging |
| VNA (Very Narrow Aisle) | Q235B / Q355B Steel | High (Narrow Aisle 1.6m) | 100% Direct Picking | -10°C to +45°C | High-Bay Raw Material Hubs & Central Dispensaries |
| Coldroom Drive-In Racking | Hot-Dip Galvanized / Q235B | High (LIFO Storage) | LIFO (Last-In, First-Out) | -40°C to +30°C | Frozen Plasma, Active Ingredients, Deep Freeze |
| Automated AS/RS High-Bay | Q355B High Tensile Steel | Maximum Vertical Density | Software Controlled FIFO | -35°C to +45°C | 24/7 Fully Automated Cleanroom & Distribution Hubs |
Future Procurement Trends in Pharmaceutical Warehousing (2025–2035)
The global pharmaceutical logistics market is undergoing a structural transition driven by biological therapies, personalized medicine, strict temperature tracking regulations, and labor constraints. Procurement directors and warehouse automation engineers must anticipate three major operational shifts when specifying warehouse racking infrastructure:
1. Sub-Zero Cold-Chain Escalation
Next-generation mRNA vaccines, cell therapies, and biopharmaceuticals demand continuous storage temperatures between -20°C and -80°C. Procurement teams are moving away from standard painted steel toward heavy-duty hot-dip galvanized racking and specialized cold-resistant alloy steels (Q355B) that eliminate hydrogen embrittlement and coating failure under deep sub-zero thermal cycling.
2. Full-Height AS/RS Integration
Urban industrial space scarcity and high cleanroom HVAC operational costs are driving pharmaceutical facilities upward. High-bay AS/RS systems reaching heights of 25 to 40 meters maximize floor utilization. Racking procurement now focuses heavily on millimeter-level beam vertical tolerance, dynamic deflection coefficients, and seamless integration with stacker cranes and WMS software.
3. Strict Cleanroom Surface Standards
Regulatory agencies (FDA, EMA, NMPA) are auditing cleanroom micro-particulate contamination more intensely. Storage racks installed within ISO Class 7 or Class 8 cleanrooms must feature ultra-smooth, non-porous powder coatings with anti-microbial additive layers, rounded profile geometries that prevent dust accumulation, and flush bolted joints to allow fast chemical washdowns.
Racking System Development & Manufacturing Technology Trends
The evolution of industrial storage racking is powered by advanced steel metallurgy, robotic manufacturing automation, and digital twin monitoring systems. ApexDrive Racking leads the market by implementing state-of-the-art production technologies across our 20,000+ m² manufacturing complex:
-
Precision German Roll-Forming Lines: Our multi-stage continuous roll-forming machinery profiles high-tensile Q355B steel into complex upright geometries with up to 18 cold-bent deformation angles. This profile geometry increases torsional stiffness by 35% compared to basic omega profiles while keeping structural weight optimal.
-
Robotic Manipulator Arc Welding: Manual welding introduces human error, porosity, and uneven thermal strain. ApexDrive utilizes fully automated robotic welding manipulators to attach beam connectors. Robotic welding guarantees 100% seam penetration, uniform weld beads, zero slag entrapment, and superior fatigue resistance during repeated forklift loading cycles.
-
220-Meter Automated Swiss Gema Coating System: Our 10-stage surface pretreatment line includes automatic degreasing, acid rust removal, silane passivating wash, and high-voltage electrostatic powder spraying using Swiss Gema guns. Powder coated components undergo curing at a constant 180°C to form an impact-resistant, chemical-proof barrier averaging 60 to 90 microns in thickness.
-
IoT Sensor & Seismic Structural Monitoring Ready: Modern high-bay pharmaceutical installations can be outfitted with embedded tilt sensors, strain gauges, and wireless load cells. These sensors communicate real-time structural health data to facility management dashboards, providing early warnings for minor upright impacts or unexpected overload distribution.
Enterprise Advantages & Global OEM/ODM Engineering Capabilities
ApexDrive Industrial Racking Co., Ltd. (established in September 2006 in Nanjing, China) has grown into a globally recognized manufacturing authority in industrial storage systems. Operating two state-of-the-art production bases (Jiangning Factory & Pukou Factory), we combine rigorous structural engineering with flexible OEM/ODM manufacturing customization.
Verified Raw Material Traceability
We build exclusive supply contracts with China's largest steel producers: Baosteel, Masteel, and Wuhan Iron and Steel. Every coil batch is supplied with certified mill test reports detailing exact carbon content, chemical composition, and yield strength testing (Q235B & Q355B structural grades).
ISO 9001:2015 & CE Certification
Our manufacturing workflow operates under certified ISO 9001:2015 quality management procedures. Our racking systems carry full CE marking certification, ensuring compliance with European structural safety standard EN 15512 and FEM 10.2.02 codes for industrial steel racking.
Export Packaging & Global Shipping
Export racking components undergo specialized sea-freight bundling. Uprights and beams are secured with multi-tier heavy steel strapping and protective plastic wrapping. Connecting brackets, safety pins, and grade 8.8 structural bolts are packed in reinforced cartons on solid plywood pallets for safe container unloading.
Frequently Asked Questions for Pharmaceutical Racking Procurement
Technical guidance and planning answers from our senior warehouse storage engineering team.
What specific warehouse dimensions and engineering data are needed to design a pharmaceutical racking layout?
To generate an optimized CAD warehouse layout and load capacity calculation report, our engineering team requires: (1) Building architectural CAD files showing clear height under trusses, floor slab load capacity (kN/m²), column grids, door locations, and fire sprinkler clearances; (2) Pallet unit load specifications including length, width, height, and maximum gross weight per pallet; (3) Number of SKUs, required total pallet positions, and inventory rotation rules (FIFO vs. LIFO); (4) Material handling equipment specs including forklift model, turning radius, maximum lift height, and mast height. We provide complete layout drawings and load design reports free of charge.
How do your pharmaceutical pallet racking systems comply with CE and EN 15512 standards?
Our steel pallet racking systems are engineered according to European Standard EN 15512 (Steel static storage systems - Adjustable pallet racking systems - Principles for structural design). We utilize structural Q235B and Q355B cold-formed steel with certified yield strengths. Structural calculations account for dead load, live pallet load, placement impact factors, frame sway deflection, and seismic acceleration. CE certification validates that our design methodology, raw material sourcing, and factory production control meet stringent European safety directives.
What surface treatment option is best for sub-zero pharmaceutical cold storage (-25°C to -40°C)?
For sub-zero cold rooms, cold storage vaccine distribution centers, and deep-freeze facilities, we recommend Hot-Dip Galvanizing (HDG) or specialized low-temperature electrostatic powder coating over passivated steel. Hot-dip galvanizing coats components in a 65–85 micron molten zinc layer inside and out, offering decades of maintenance-free corrosion resistance down to -40°C without risk of paint flaking, micro-cracking, or rust formation caused by moisture condensation during defrost cycles.
What support do you offer for overseas racking installation and site management?
Every international shipment includes detailed 3D assembly drawings, component coding tags, and comprehensive English installation manuals. Our engineering department provides live remote video guidance and technical support during site setup. For large-scale automated warehouses, high-bay AS/RS systems, or multi-tier mezzanine projects, ApexDrive can dispatch experienced installation supervisors or full installation crews to oversee turnkey project assembly anywhere worldwide.
How do radio shuttle racking and AS/RS compare for pharmaceutical high-density storage?
Radio shuttle racking uses battery-powered semi-automated shuttles to carry pallets inside deep channels (up to 40m deep), driven by standard forklifts at the aisle face. It is ideal for batch-controlled products requiring deep-lane storage with high volume per SKU. Automated Storage and Retrieval Systems (AS/RS) replace forklifts entirely with computer-guided stacker cranes and conveyor systems linked to WMS/WCS software. AS/RS provides maximum height utilization (up to 40 meters), 24/7 unmanned cleanroom operation, zero picking errors, and complete real-time batch traceability required for strict GDP compliance.
Request a Free Engineering Layout & Project Quote
Connect directly with our senior warehouse racking engineers. We provide CAD layout design, structural load calculations, and factory-direct pricing within 24 hours.
Inquire Now