ApexDriveRACKING
Factory Showcase
Featured Heavy-Duty Racking & Automated Storage Systems
Engineered specifically for heavy industrial payloads, chemical drum containment, cold-chain environments, and automated intralogistics.
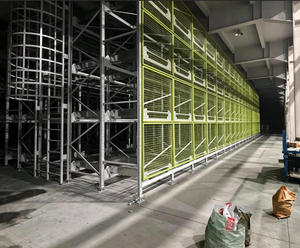
Kaku ASRS Smart Pallet Racking 6-Layer Automated System (1300kg Cap.)
Galvanized corrosion-resistant structural steel for automated chemical and drum dispatching.
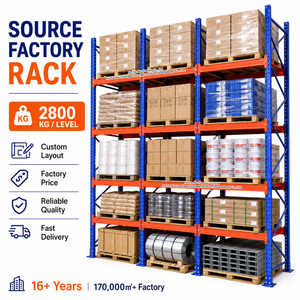
2800KG 5 Levels High Bay Industrial Heavy Duty Pallet Racking System
Ultra-heavy loading profile designed for high-density vertical drum cradles and palletized liquids.
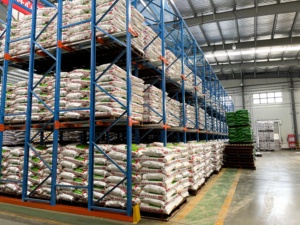
Heavy Duty Radio Shuttle Racking for Cold Storage & Liquid Cargo
Semi-automated deep-lane pallet runner engineered for hazardous liquid temperature stability.
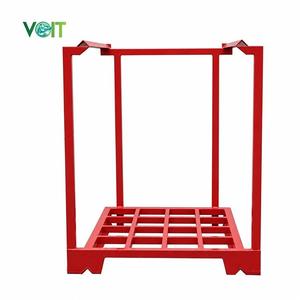
Industrial Storage 1000kg Metal Nestainer Stacking Rack System
Portable modular nesting frames optimized for bulk raw material drum transport and storage.
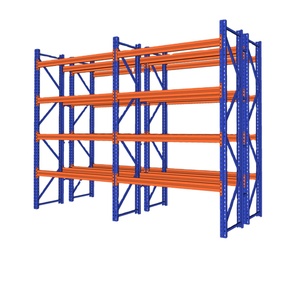
Heavy Duty Modular Pallet Storage Frame with Spill Catching Support
Interlocking upright structural beams for adaptable industrial manufacturing operations.
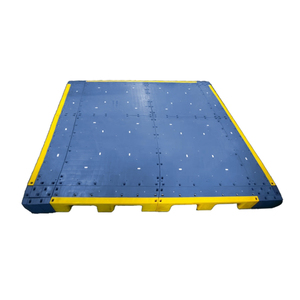
Oversize Heavy Duty Closed Deck HDPE Pallet Platform (2500x2500mm)
Corrosion-proof chemical-resistant base deck engineered for multi-drum pallet loads.
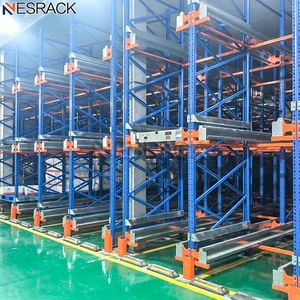
Semi-Automatic High Density Radio Shuttle Pallet Racking System
Remote-controlled channel shuttle system optimizing drum storage density by up to 80%.
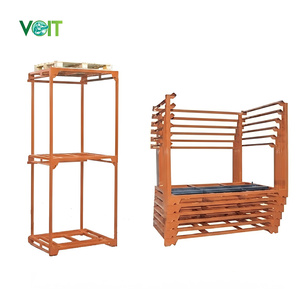
Cost Effective Detachable Heavy Duty Stackable Drum Racking Pallet
Flexible knockdown steel post racking system for dynamic drum logistics and staging.
20,000 m²
Manufacturing Infrastructure
30,000 T
Annual Steel Production
6,000+
Global Projects Installed
ISO / CE
Certified Quality Control
Technical Whitepaper
Engineering & Sourcing Standards for Industrial Drum Pallet Racking
In modern chemical processing, petroleum refining, pharmaceutical synthesis, and bulk liquid distribution, securing industrial liquid drums—specifically standard 55-gallon (200-liter) steel and HDPE drums—demands structural precision far beyond conventional warehouse pallet racking. Liquid payloads exhibit dynamic hydraulic surge, localized high concentrated stress, and severe environmental hazards in the event of containment breach. Selecting the right China drum storage pallet racking factories and supplier is not merely a logistics procurement decision; it is a paramount environmental safety and structural compliance directive.
Information Gain Insight: Unlike static boxed cargo, palletized drums store dense liquid masses (typically 200kg to 300kg per drum, totaling 800kg–1200kg per 4-drum pallet). Standard beam deflection limits (L/200) are insufficient for drum storage. China's top racking engineers enforce structural beam stiffness targets of L/300 to L/400 under maximum load, paired with custom drum cradles, integrated spill-containment sumps, and seismic anchor lockups.
1. Structural Load Mechanics & Material Specifications
China’s leading racking manufacturers utilize high-grade structural steel coil sourced directly from tier-1 state mills such as Baosteel, Masteel, and Wuhan Iron and Steel. Understanding the metallurgical distinction between structural grades is essential for long-term safety:
Q235B Cold-Rolled Carbon Steel
Yield Strength: ≥235 MPa | Tensile Strength: 370–500 MPa. Ideal for standard selective pallet racking, vertical storage cradles, and medium-bay warehouse installations under non-extreme environmental ambient conditions.
Q355B High-Strength Structural Steel
Yield Strength: ≥355 MPa | Tensile Strength: 470–630 MPa. Specified for heavy-duty high-bay AS/RS systems, deep-lane radio shuttle drum channels, and high-seismic risk regions where column buckling resilience is mandatory.
2. Spill Containment & Chemical Safety Compliance (NFPA 30 / OSHA 1910.106)
When racking flammable, combustible, or hazardous corrosive chemical drums, international safety codes mandate secondary containment engineering. Premier Chinese manufacturers integrate compliant secondary containment mechanisms directly into the rack design architecture:
- Integrated Sump Trays: Continuous heavy-gauge galvanized or epoxy-coated steel catchment basins positioned beneath drum levels, providing a minimum containment capacity of 110% of the largest single container or 25% of the total volume stored per bay (per EPA 40 CFR 264.175 standards).
- Horizontal Drum Cradles: Specialized welded profile saddles that secure 55-gallon drums horizontally, preventing roll displacement while allowing integrated gravity-dispensing taps.
- Flame-Retardant Surface Finishing: Electrostatic powder coating cured at 180°C to 200°C on automated 220-meter processing lines, delivering anti-static, spark-resistant, and chemical-corrosion barrier properties.
Technical Comparison
Drum Storage Racking Systems Selection Matrix
Evaluate technical parameters across major racking formats to match your facility throughput and density goals.
| Racking Architecture | Storage Density | Direct Selectivity | Spill Containment Ease | Handling Equipment | Ideal Industrial Application |
|---|---|---|---|---|---|
| Selective Drum Pallet Rack | Standard (60%) | 100% Direct Access | High (Individual Sump Trays) | Standard Counterbalance / Reach Truck | High SKU variety, chemical distribution hubs |
| Radio Shuttle Drum Racking | Very High (85%) | FIFO / LIFO by Lane | Medium (Channel Catchment) | Automated Radio Runner + Forklift | Cold storage, high-volume batch chemical production |
| Automated AS/RS Stacker Crane | Maximum (95%) | 100% Computerized Access | High (Systemic Drainage Sensing) | Automated Stacker Crane / WMS System | 24/7 continuous smart chemical manufacturing plants |
| Portable Stacking Nestainer | Flexible Dynamic | Block Stacking Access | Integrated Base Pallet Catch | Standard Forklift Truck | Seasonal raw material buffer zones & temporary staging |
Manufacturing Excellence
Controlled Production: From Steel Coil to Export Container
Our 20,000 m² modern production facility executes end-to-end quality control across six dedicated production phases.
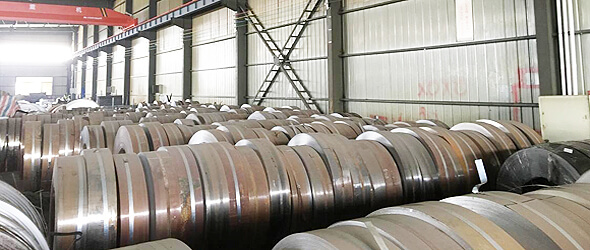
Phase 01
Traceable Raw Material Procurement
Every batch of Q235B and Q355B steel is accompanied by official steel mill test certificates (MTC). Thickness, yield point, and chemical composition are verified prior to uncoiling.
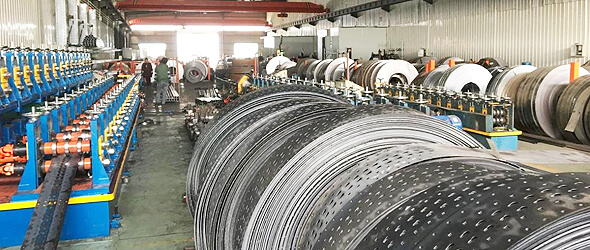
Phase 02
Precision Continuous Roll-Forming
Utilizing German-designed multi-pass continuous cold roll-forming lines, upright profiles up to 12 meters are formed in a single stroke with cumulative pitch tolerances within ±2 mm.
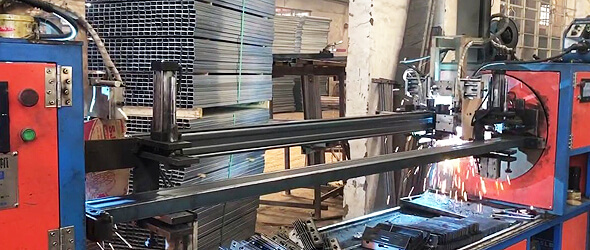
Phase 03
Automated Robotic Arm Welding
Beam connectors, heavy-duty footplates, and drum cradles are welded using automated multi-axis robotic manipulators, guaranteeing full penetration, zero porosity, and uniform structural joints.
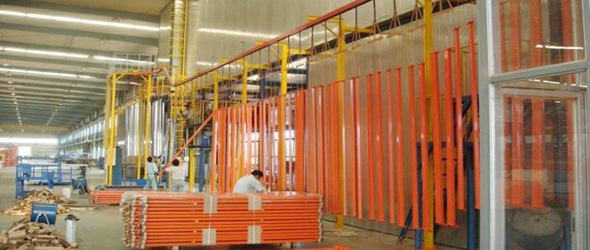
Phase 04
10-Stage Surface Pretreatment & Powder Coating
Components pass through a 10-stage cleaning, degreasing, and phosphating tunnel before receiving electrostatic powder application via Swiss Gema guns and 180°C thermal curing.
Industry Insights
Global Sourcing & Future Trends in Industrial Drum Storage
IoT & Smart Leakage Monitoring Integration
Next-generation chemical drum racking incorporates early-warning optical and conductivity sensors within spill sumps, sending real-time alarm telemetry to warehouse WMS networks.
Fully Automated AS/RS Heavy Drum Logistics
Rising labor costs and stringent hazardous-material handling safety rules are accelerating the transition from manual forklift drum handling to stacker cranes and AGVs.
Modular Modular Sump & Grid Customization
Suppliers are standardizing drop-in modular sumps and interchangeable drum cradles, allowing standard selective pallet racks to be retrofitted for hazardous drum duty rapidly.
Enterprise Strength
ApexDrive Industrial Racking Co., Ltd.
Established in September 2006, ApexDrive Industrial Racking Co., Ltd. is a premier Chinese manufacturer specializing in heavy-duty storage racking, radio shuttle systems, mezzanine steel platforms, and automated AS/RS high-bay logistics equipment.
Operating from our 20,000 square meter factory base equipped with 150+ automated production machines, we deliver certified structural storage products compliant with ISO 9001:2015 and European CE safety standards for international buyers worldwide.
ISO 9001:2015
Certified Quality Management System
CE Certified
European Structural Safety Compliance
Free CAD Design
Engineering & Load Calculation
Global Installation
Manuals, Video & On-Site Support
Purchasing FAQ
Frequently Asked Questions for Overseas Buyers
Detailed technical and logistical insights to streamline your drum racking procurement process.
What critical parameters are required to engineer a custom drum storage racking layout?
To engineer an optimal drum racking system, our engineering team requires: (1) Drum dimensions (e.g., standard 55-gallon steel or polyethylene drum height and diameter); (2) Palletized configuration (2-drum or 4-drum layout per pallet) and gross weight per unit load; (3) Liquid properties (flammability, corrosiveness, viscosity) to determine spill containment sump volume and powder coat chemical resistance; (4) Warehouse CAD layout showing clear height, column grid, door clearance, and sprinkler drop locations; and (5) Handling equipment parameters (forklift lift height, aisle width, turning radius).
How is secondary spill containment calculated for chemical drum racking?
In accordance with EPA 40 CFR 264.175 and NFPA 30 guidelines, secondary containment sumps located at the base or individual levels of drum racking must hold at least 110% of the volume of the largest single container stored, or 25% of the total aggregate volume of all containers in the bay, whichever is greater. Our engineering team calculates exact liquid sump capacity and integrates removable galvanized grating for effortless spill clean-up.
What steel grades and anti-corrosion treatments are recommended for chemical environments?
Main structural uprights and load beams are roll-formed from Q235B or Q355B structural steel. For standard warehouses, a 10-stage chemical pretreatment followed by electrostatic epoxy-polyester powder coating (cured at 180°C–200°C) offers excellent durability. For harsh acidic, alkaline, or outdoor environments, we provide hot-dip galvanizing (HDG) per ISO 1461, creating a protective zinc coating thickness of 60–80 microns that prevents rust for decades.
How are heavy-duty racking orders packaged to prevent export transit damage?
Racking upright frames and load beams are bundled with multi-tier heavy steel strapping, separated by plastic protective spacers and wrapped in industrial stretch film. Small accessories, safety pins, frame anchor bolts, and drum cradles are packed in heavy-duty corrugated cartons secured to export-grade plywood pallets. Every bundle features clear bilingual packing lists to accelerate customs clearance and on-site sorting.
Does ApexDrive provide overseas installation guidance and technical support?
Yes. Every project ships with detailed CAD installation assembly drawings, component load reports, and step-by-step English instruction manuals. Our project engineers provide 24/7 remote video support. For large-scale automated AS/RS or multi-tier mezzanine installations, we can dispatch experienced installation supervisors directly to your project site.
What is the difference between horizontal drum cradles and vertical drum pallet racking?
Vertical drum pallet racking stores drums upright on standard pallets, utilizing specialized wire decking or heavy-duty crossbeams; it maximizes storage density and allows 4-drum pallet handling. Horizontal drum cradles store drums laying on their sides on dedicated saddle supports; this is ideal for facilities requiring direct gravity dispensing or decanting of chemical liquids directly while the drum remains safely stored in the rack bay.
Ready to Optimize Your Industrial Drum Storage Facility?
Contact our senior engineering team today for a free warehouse CAD layout, load capacity calculation report, and competitive factory-direct quote.
Get a Quote