ApexDriveRACKING
Engineered Mobile & Industrial Racking Systems
Direct Factory Production | ISO 9001:2015 & CE Certified | Custom Structural Calculations
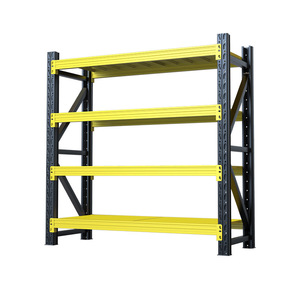
Light-duty High Capacity Storage Racks for E-commerce Warehouses, Multi-layer Adjustable Storage Hardware Racks
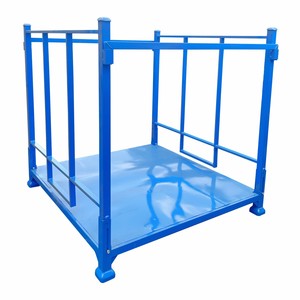
Manufacturer Custom Portable Stacking Racks with Steel Pallet Base & Removable Corner Posts for Cold Chain Logistics
Heavy Duty Drive Rack Warehouse Storage System High Density Pallet Racking Solution Structural Steel 1200kg LIFO Storage
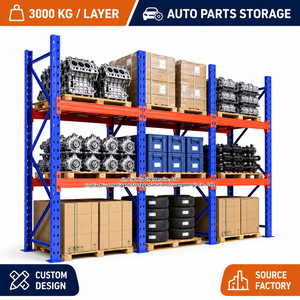
200-4000KG Selective Pallet Racking Heavy Duty Warehouse Rack Custom Size OEM Manufacturer
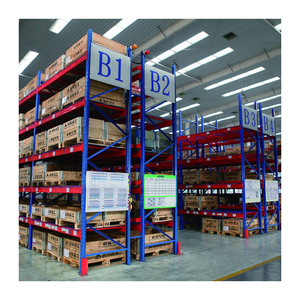
Industrial Pallet Racking System Spliced Steel Drop-Over Deck Panel Warehouse Storage Rack 2000kg Heavy Duty
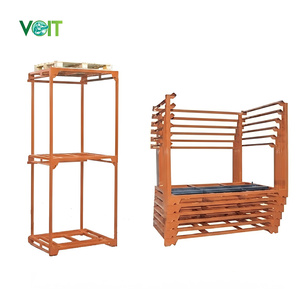
Cost Effective Heavy Duty Warehouse Industrial Detachable Stackable Racking Pallets
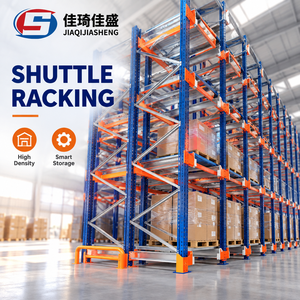
Custom Project Planning Service OEM ODM Stable Operation Intelligent Shuttle Rack for E-commerce Fulfillment

3000KG Heavy Duty Warehouse Shelf Rack for Pallet and Carton Storage 4 Levels for Pallet Storage
20,000+
Sqm Manufacturing Base
30,000T
Annual Steel Output
6,000+
Global Racking Projects
±2mm
Precision Roll-Forming
Industrial Technical Whitepaper: Mobile Pallet Racking Systems
Structural Integrity, Mechanical Automation, and Global Procurement Strategies
1. Executive Overview & Search Intent Baseline
Modern warehouse logistics require unprecedented floor space optimization, particularly as industrial real estate costs escalate globally and cold storage energy consumption demands strict volume compaction. When sourcing from China's best mobile pallet racking factories, procurement directors, logistics architects, and warehouse operators must look beyond basic price-per-ton metrics to evaluate engineering integrity, control system reliability, anti-seismic resistance, and structural steel compliance (EN 15512, FEM 10.2.07, and ANSI MH16.1 standards).
Mobile Pallet Racking Systems—specifically Electric Mobile Pallet Racking (EMPR)—represent the pinnacle of high-density accessible storage. Unlike fixed selective pallet racking, which requires multiple static working aisles, mobile pallet racking mounts heavy-duty structural upright frames onto electrically driven mobile bases (carriages) that travel along floor-embedded steel guide rails. By opening a single working aisle on demand via PLC automation or remote radio control, EMPR increases storage capacity by up to 85% to 100% within the same physical footprint, while retaining 100% direct access (selectivity) to every single pallet location.
Engineering Insight: Information Gain & Structural Load Distribution
The structural load dynamics of mobile pallet racking differ fundamentally from static racking. Because entire racking banks (weighing up to 300 metric tons per mobile block) move dynamically along floor rails, dynamic acceleration forces, brake torque, and slab floor deflection must be factored into structural steel grade selections (Q235B vs. Q355B structural steel profiles).
2. Structural Mechanics & Electrical Base Engineering
A high-performance mobile pallet racking installation manufactured in leading Chinese OEM facilities consists of three key engineering sub-assemblies:
Superstructure Racking
Roll-formed or hot-rolled structural steel uprights engineered from prime Q355B grade coil steel. Featuring variable beam profile hook connections with safety pins preventing accidental dislodgement under high-velocity forklift operations.
Motorized Carriages
Heavy-duty steel wheel carriages fitted with direct-drive gear motors, soft-start vector frequency converters (VFDs), and heavy-load forged steel wheels running on precision ground embedded floor rails.
Integrated Safety Matrix
Dual-laser photo-electric optical safety barriers scanning both floor level and vertical faces, emergency stop push-buttons, proximity sensors, and anti-collision bumpers ensuring full CE compliance and zero operator hazards.
When evaluating China mobile pallet racking factories, engineering teams must review the roll-forming precision of upright sections. Premium facilities utilize automated multi-station cold roll-forming lines imported with German or Swiss tooling, capable of producing continuous upright columns up to 12 meters in length without mid-span splicing. Cumulative hole pitch tolerance must be held strictly within ±2 mm over a 12-meter span to ensure perfectly plumb assembly and even load distribution across carriage wheel bearings.
3. Technical Comparative Matrix: Racking Architectural Systems
Choosing the correct storage topology requires balancing initial Capital Expenditure (CAPEX), operational throughput, space utilization, and SKU management requirements. The matrix below contrasts Electric Mobile Pallet Racking against other mainstream industrial warehouse systems:
| Storage Topology | Space Utilization | Direct Selectivity | Relative CAPEX | Cold Chain Suitability | Handling Equipment |
|---|---|---|---|---|---|
| Electric Mobile Racking (EMPR) | Very High (85-90%) | 100% Direct Access | Medium - High | Optimal (-30°C Ready) | Standard Counterbalance / Reach Truck |
| Selective Pallet Racking | Low (40-45%) | 100% Direct Access | Low | Moderate (High Energy Overhead) | Standard Forklift |
| Drive-In Racking | High (70-75%) | Low (LIFO Only) | Low - Medium | Good | Specialized Narrow Forklift |
| Radio Shuttle Racking | Very High (80-85%) | Moderate (FIFO/LIFO Lane) | Medium | Excellent | Standard Forklift + Battery Shuttle |
| Automated Storage & Retrieval (AS/RS) | Maximum (95%+) | 100% Automated | Very High | Excellent | Automated Stacker Cranes / WCS |
4. Manufacturing Capabilities & Steel Powder Coating Standards
Top-tier manufacturing enterprises in China, such as ApexDrive Industrial Racking, differentiate themselves through raw material sourcing and surface treatment metallurgy. Low-cost vendors often compromise by using second-grade commercial steel with high thickness tolerances and inconsistent yield strength.
A. Structural Steel Metallurgy (Q235B vs. Q355B)
Primary load-bearing components (uprights, beams, and carriage structural frames) are crafted from verified structural steel coils procured directly from state-owned steel mills including Baosteel, Masteel, and Wuhan Iron and Steel (WISCO). Mill test certificates (MTC) according to EN 10204 3.1 accompany every production batch.
- Q235B Grade Steel: Yield strength $f_y \ge 235 \text{ MPa}$, tensile strength $R_m = 375\text{--}500 \text{ MPa}$. Ideal for standard selective beams and light-to-medium shelf panels.
- Q355B Grade Steel: Low-alloy high-strength steel with yield strength $f_y \ge 355 \text{ MPa}$, tensile strength $R_m = 470\text{--}630 \text{ MPa}$. Specified for heavy-duty mobile carriages, tall high-bay uprights (over 8 meters), and high-load cantilever arms to reduce weight while preserving dynamic safety factors.
B. Surface Treatment & Powder Coating Line Specifications
Corrosion resistance is paramount, especially in cold storage facilities operating at sub-zero temperatures where condensation occurs during defrost cycles. Qualified Chinese factories operate continuous, 220-meter automated electrostatic powder coating lines equipped with Swiss Gema spraying heads. The 10-stage pre-treatment process includes:
- Hot chemical degreasing and oil removal
- High-pressure water rinse & de-scaling
- Surface activation and nano-ceramic / zirc-phosphate coating formation
- Deionized water final rinse
- Drying oven moisture elimination at 110°C
- Electrostatic powder application (thermosetting epoxy-polyester powder)
- High-temperature curing tunnel maintaining 180°C–200°C for 20 minutes
This process yields a dry film coating thickness of 60 to 90 microns with cross-hatch adhesion meeting Class 0 standards (ISO 2409) and salt spray resistance exceeding 500 hours (ASTM B117).
5. Technological Development Trends (2025–2030)
As smart logistics and Industry 4.0 transform warehouse automation, China's best mobile pallet racking factories are pioneering technological shifts in several key domains:
WMS/WCS & AMR Native Integration
Modern mobile racking systems are no longer isolated mechanical islands. Advanced installations interface directly with Warehouse Control Systems (WCS) via CANbus or Industrial Ethernet over Wi-Fi. When an Autonomous Mobile Robot (AMR) or AGV approaches, the WCS automatically commands the mobile racking bank to open the required aisle in advance, eliminating forklift waiting latency.
IoT Structural Strain & Deflection Sensors
Real-time IoT tilt and load sensors embedded into critical upright bases monitor structural beam deflection and column tilt caused by uneven floor settlement or accidental forklift impacts. Telemetry alerts maintenance personnel before structural fatigue thresholds are breached.
Furthermore, energy-efficient regenerative braking drives in mobile carriages capture kinetic energy during decelerations, feeding power back into the warehouse grid and lowering overall electrical OPEX in large-scale logistics hubs.
6. Global Sourcing & Implementation Engineering Roadmap
Successfully procuring heavy-duty mobile pallet racking from Chinese manufacturers requires a structured, multi-phase engineering protocol to ensure on-time delivery and zero installation errors on site:
Phase 1: Civil & CAD Survey
Provision of architectural floor slab drawings (concrete compressive strength C30/C37 minimum, F-number flatness FF50/FL45), overhead column grid locations, sprinkler clearance height, and pallet load profiles ($W \times D \times H$ and unit weight).
Phase 2: FEA & Layout Simulation
Engineers run Finite Element Analysis (FEA) software to calculate sway stability, seismic resistance up to Magnitude 7.0, beam deflection limits ($L/300$), and rail bed foundation load distribution points.
Phase 3: Trial Assembly & QC
Prior to containerization, trial assemblies of mobile carriage wheel blocks, drive shafts, motor mountings, and beam connectors are performed at the factory to verify mechanical tolerances.
Export Packaging & Shipping Safeguards
Uprights and beams are bundled with multi-tier high-tension steel strapping, heavy protective plastic film, and timber spacers. Smaller components (bolts, safety pins, footplates, control panels) are packaged in reinforced export cartons secured to sea-worthy plywood pallets. Clear English labelling on every bundle accelerates customs clearance and simplifies on-site material sorting.
Frequently Asked Questions (Procurement FAQ)
Expert Engineering Insights for Warehouse Importers & System Integrators
What floor specification is required to install heavy-duty Electric Mobile Pallet Racking?
Mobile racking systems impose concentrated wheel loads on the floor slab. The concrete floor slab typically requires a minimum compressive strength of C30/C37 with steel reinforcement. Floor flatness must adhere to DIN 18202 or VDMA standards (e.g., maximum floor level variance under 2 mm per meter span). Ground rails can be embedded during new floor construction or retro-fitted into chased channels in existing concrete slabs using non-shrink epoxy grout.
How do mobile pallet racking systems perform in cold storage and freezing conditions?
Mobile pallet racking is the preferred high-density solution for cold storage environments down to -30°C. By eliminating unused aisles, cold room volume is reduced by up to 45%, significantly lowering refrigeration energy bills. Electrical components used in cold storage feature IP65 heating elements in PLC control cabinets, low-temperature synthetic lubricants in drive gearboxes, and specialized cold-drawn Q355B steel profiles resistant to low-temperature embrittlement.
What safety mechanisms prevent personnel or forklifts from being crushed inside an aisle?
Safety compliance is paramount. Modern mobile racking systems incorporate multi-layer redundant safety mechanisms: (1) Floor-level optical safety light curtains that trip and stop movement instantly if a foot or obstacle enters an active aisle; (2) Vertical optical safety barriers scanning the aisle entrance; (3) Mechanical emergency stop buttons mounted on every carriage console; and (4) Motor overload torque sensors that halt movement upon detecting resistance.
How does an overseas buyer manage installation and commission of Chinese racking?
Leading manufacturers provide complete installation documentation, step-by-step 3D assembly CAD drawings, component tagging, and video tutorials. For complex or large-scale projects, factories can dispatch senior structural and electrical field engineers to supervise local installation crews, perform rail alignment calibration, configure PLC control logic, and certify system handover.
What is the typical production lead time and container shipping capacity?
Standard manufacturing lead times range from 20 to 35 days depending on total tonnage and custom electrical requirements. A standard 40-foot High Cube (40HC) sea container can hold approximately 20 to 23 metric tons of steel racking components. Bundles are designed specifically to maximize container volume utilization and allow rapid unloading with standard fork trucks.
Partner with China's Premier Racking Factory
From initial warehouse CAD layout design and structural load calculation to precision manufacturing, export packing, and international commissioning support—ApexDrive Industrial Racking delivers certified engineering quality for your logistics facility.
Project Engineering Checklist
- 100% Free Architectural CAD Layout Planning
- Structural FEA & Seismic Loading Calculations
- Baosteel & Masteel Certified Raw Materials
- ISO 9001:2015 & CE Structural Certification
- On-demand Online Engineering Consultation