ApexDriveRACKING
Featured Industrial Storage Systems
Factory-direct engineered racking and semi-automated shuttle equipment compliant with ISO 9001:2015 and CE standards.
Heavy Duty Pallet Rack System Steel Storage Rack Industrial Easy Assembly Adjustable for Bulk Storage
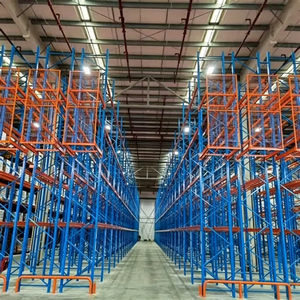
All Bolt Assembly Structure Easy Disassembly and Relocation High Density Double Deep Rack Double Deep Pallet Racking
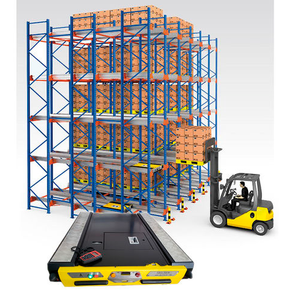
Adjustable Semi-automatic Warehouse Storage Rack Pallet Shuttle Racking System Radio Shuttle Storage System Stacking Shelves
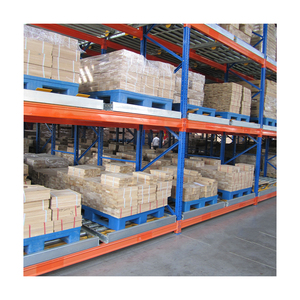
Steel Pallet Rack System Heavy Shelving Storage Shelf Selective Heavy Duty Rack Steel Shelving Warehouse Racking For Wholesale
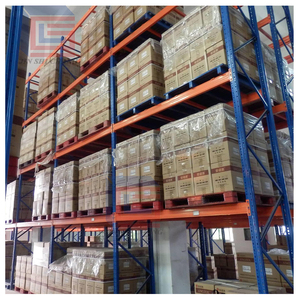
Industrial Heavy Duty Steel Pallet Rack Warehouse Shelving System For Storage, Distribution Center And Factory Use
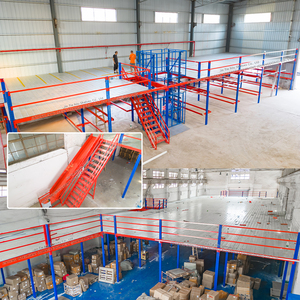
Second Floor System Mezzanine Steel Elevated Storage Platform For Factory Warehouse Organization Up To 500kg/sqm
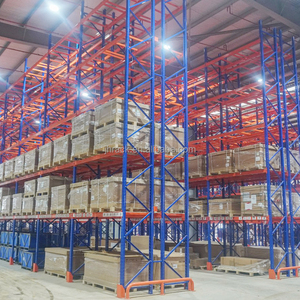
Heavy-Duty Corrosion Protected Pallet Racking Systems For Warehouse And Factory Storage By Jinhui Warehousing Suppliers
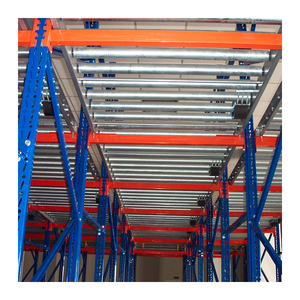
Pallet Flow Rack High Quality Fifo Warehouse Storage Racks Gravity Pallet Flow Racking First In First Out Rack System
Manufacturing Scale & Global Engineering Performance
Direct OEM/ODM production credentials supporting supply chains across North America, Europe, Southeast Asia, and the Middle East.
20,000+
Sqm Manufacturing Base
30,000+
Tons Annual Output
150+
Precision Machinery Sets
6,000+
Global Projects Installed
Technical Whitepaper: Engineering Automated Pallet Shuttle Systems
Understanding structural integrity, control logic, battery chemistry, and ROI mechanics in high-density automated warehousing.
In modern industrial logistics, floor space optimization and operational throughput are critical vectors driving competitive advantage. As a premier **China Wholesale Automated Pallet Shuttle System Manufacturer & Exporter**, ApexDrive Industrial Racking Co., Ltd. delivers high-density storage solutions engineered to convert underutilized vertical warehouse volume into hyper-efficient storage assets. By eliminating interior forklift access aisles required in traditional selective racking, radio pallet shuttle technology increases pallet storage capacity by up to 80% while dramatically accelerating loading and retrieval cycle times.
1. System Architecture: How Automated Radio Shuttle Racking Works
An automated radio pallet shuttle system is a self-powered semi-automated deep-lane storage solution. The core infrastructure consists of heavy-duty structural steel racking, precision-rolled guide rails, and autonomous battery-driven shuttle carts controlled via handheld RF remotes or integrated Warehouse Management System (WMS) networks.
The operational sequence operates seamlessly:
- Step 1 (Placement): A standard forklift deposits the automated shuttle car onto the precision guide rails of the designated storage channel.
- Step 2 (Load Input): The forklift places a loaded pallet onto the entry position of the channel rails.
- Step 3 (Autonomous Transit): Guided by integrated optical sensor arrays and laser distance meters, the shuttle cart lifts the pallet vertically off the rail surface and transports it smoothly to the deepest available storage location.
- Step 4 (Return & Repetition): The cart lowers the unit load onto the rail supports and returns autonomously to the front position, awaiting the next pallet.
Information Gain: Dual Inventory Flow Control (FIFO vs. LIFO)
Unlike traditional Drive-In racking systems that force strict Last-In, First-Out (LIFO) material movement, an engineered automated shuttle racking system can be configured for both **LIFO and FIFO (First-In, First-Out)** operations. In FIFO mode, loading occurs at one end of the channel while retrieval takes place at the opposite end. This flexibility makes radio shuttle racking ideal for cold chain facilities, food and beverage distribution, and fast-moving consumer goods (FMCG) requiring strict expiration batch tracking.
Heavy Payload Capacity
Engineered to handle unit loads ranging from 500 kg up to 1,500 kg per pallet, with custom heavy-duty shuttles rated up to 2,000 kg for metal casting and chemical bulk applications.
LiFePO4 Power Management
Powered by industrial Lithium Iron Phosphate batteries providing 8 to 10 hours of continuous operation with rapid 3-hour fast-charging dock systems and zero memory effect.
Cold Storage Ready
Specialized sub-zero thermal protection packages allow flawless shuttle operation inside deep-freeze warehouses down to -25°C (-13°F) without electronic failures.
2. Manufacturing Rigor & Structural Integrity: The ApexDrive Standard
As an established OEM manufacturer operating from Nanjing, China, our manufacturing facilities turn raw steel into high-precision storage systems. Structural failure in high-density storage can lead to catastrophic inventory loss; therefore, we implement strict metallurgical and roll-forming quality assurance protocols.
We source prime **Q235B and Q355B structural steel coils** exclusively from premier domestic state-owned mills, including Baosteel, Masteel, and Wuhan Iron and Steel Corporation. Every raw coil delivered to our factory undergoes dimensional thickness verification and chemical tensile strength testing against factory mill certificates before entering production.
| Technical Specification | ApexDrive Standard Value | Engineering Advantage |
|---|---|---|
| Structural Steel Grade | Q235B & Q355B High-Yield Steel | Higher tensile margin prevents beam sag under load |
| Upright Roll-Forming Length | Up to 12.0 Meters (Single Piece) | Eliminates structural joints in tall high-bay applications |
| Hole-Pitch Punching Tolerance | ±2.0 mm Cumulative over 12m | Guarantees perfect beam levelness and even load transfer |
| Welding Methodology | Robotic Manipulator MIG Welding | 100% full-penetration seams with zero porosity |
| Surface Treatment Process | 220m Automatic Powder Coating Line | 10-stage degreasing, rust removal & 180°C thermal curing |
| Powder Coating Brand | Swiss Gema Spray Equipment | Uniform 60–80 micron coating thickness, high impact resistance |
During the roll-forming stage, upright profiles are shaped using multi-stage roller lines designed on German tooling software. This ensures that the closed-channel geometry of our shuttle guide rails maintains rigid parallel tolerances over long deep lanes. Even a slight deviation in rail parallelism can cause shuttle wheel binding or accelerated mechanical wear; our automated CNC punching and forming guarantee rail alignment within sub-millimeter tolerances.
Future Procurement & Strategic Industry Trends (2025–2030)
Where warehouse automation is heading and how global procurement officers can future-proof their logistics operations.
1. Transition from 2D Radio Shuttles to 4D Multi-Directional Systems
While traditional 2D shuttles move forwards and backwards within a single lane, global buyers are increasingly specifying 4D multi-directional pallet shuttles. 4D shuttles can switch tracks between longitudinal and transverse lanes independently, climbing across different racking levels via integrated lifters. This shift eliminates the need for dedicated forklifts to move shuttles between levels, unlocking true unassisted 24/7 automated storage and retrieval (AS/RS).
2. Integration with Autonomous Mobile Robots (AMRs) & AGVs
The procurement trend is rapidly moving away from isolated equipment toward fully integrated warehouse ecosystems. Modern automated pallet shuttle systems are designed with standard API endpoints and PLC protocols to interface directly with Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs). In this hybrid setup, AGVs transport pallets from receiving docks to the racking face, where the radio shuttle automatically receives and stores the pallet—completely removing manual forklift drivers from the inbound cycle.
3. IoT Cloud Telemetry & Predictive Maintenance
Next-generation shuttle fleets exported from leading Chinese factories are equipped with onboard IoT modules, vibration sensors, and thermal monitors. Facility managers can monitor battery health status, wheel wear, sensor alignment, and cycle counts in real-time via cloud dashboards. Predictive maintenance algorithms alert engineers to service mechanical parts before a fault occurs, reducing unplanned system downtime to near zero.
4. Ultra-Efficient Energy Harvesting & Green Logistics
ESG compliance and carbon footprint reduction are driving warehouse equipment specifications. Advanced shuttle carts now incorporate regenerative braking systems that harvest kinetic energy during deceleration, routing charge back into the onboard battery. Combined with intelligent standby sleep modes, total electrical power consumption per pallet cycle has been reduced by over 30% compared to legacy automation platforms.
Comprehensive Storage System Technology Comparison
Evaluating density, operational speed, initial capital expenditure (CAPEX), and ongoing operating expenses (OPEX).
| Racking System Type | Storage Density | Selective Access | Forklift Risk Level | CAPEX Level | Optimal SKU Mix |
|---|---|---|---|---|---|
| Automated Radio Shuttle | Very High (80%+) | Lane-by-Lane (FIFO/LIFO) | Very Low (No entry inside rack) | Medium-High | Medium SKU count, high volume per SKU |
| Selective Pallet Racking | Low (35-40%) | 100% Direct Access | Moderate (Aisle navigation) | Low | High SKU count, low volume per SKU |
| Drive-In Racking | High (65-75%) | Strict LIFO Only | High (Forklifts drive into channels) | Low-Medium | Low SKU count, uniform bulk storage |
| VNA (Very Narrow Aisle) | Medium-High (55-65%) | 100% Direct Access | Moderate (Requires wire guidance) | Medium | High SKU count with tall clearance |
| Full AS/RS (Stacker Crane) | Maximum (85%+) | Automated Selective | Zero (Fully automated) | Very High | High volume, high vertical height (>20m) |
Why Wholesale Buyers Choose Shuttle Racking Over Drive-In Systems
Historically, warehouse operators seeking high density opted for Drive-In racking due to low initial rack material costs. However, Drive-In racking introduces major operational friction: forklifts must drive directly inside the steel structure to place or retrieve pallets. This constant ingress results in frequent rack collisions, high structural repair bills, and severe driver safety risks.
Automated shuttle racking eliminates these issues entirely. Because the forklift operator never enters the racking structure—simply setting the pallet at the lane entrance—structural rack damage drops by over 90%. Furthermore, pallet placement speeds are significantly faster because the driver does not have to slowly navigate tight rack channels.
Enterprise Advantages: Partnering with ApexDrive Racking
Why international importers, distributors, and EPC contractors choose our manufacturing hub in Nanjing, China.
1. Free Custom CAD Engineering & Load Calculation
Our experienced structural engineering team provides complimentary warehouse CAD layout designs, 3D spatial models, and finite element stress analysis reports tailored to your specific pallet dimensions, floor load capacity, and ceiling clearances.
2. Pre-Shipment Trial Assembly & Strict QC
To guarantee zero on-site installation defects, every shuttle cart order undergoes rigorous factory testing. We perform trial frame assembly, full-load shuttle transit testing on test rails, and electrical safety validation before export packing.
3. Export-Optimized Container Packaging
Racking uprights and beams are bundled using multi-tier heavy steel strapping and protective corner guards. Small components, shuttle carts, and fasteners are secured in export plywood crates to ensure damage-free transit and quick customs clearance.
Global Turnkey Installation & Technical Guidance
Every exported racking project comes with comprehensive English installation manuals, step-by-step assembly drawings, and video tutorials. For major automation projects, ApexDrive dispatches senior installation engineers and commissioning teams directly to your international project site to supervise erection, test shuttle integration, and train your local operational staff.
Frequently Asked Questions (FAQ) for Overseas Procurement
Essential guidance answered by our chief automated warehousing engineers.
1. What key warehouse parameters are required to generate a custom design and quote?
To create an accurate CAD layout and price quotation, our engineering team requires: (1) Architectural CAD floor plans or building dimensions showing clear ceiling height, column spacing, and door/sprinkler locations; (2) Pallet specifications including length, width, height, and gross weight per unit load; (3) Required inventory capacity (total pallet positions); (4) Operating environmental conditions (e.g., ambient vs. cold storage temperature); and (5) Stock rotation rules (FIFO or LIFO preference).
2. What is the expected battery operating lifetime and recharge time for the radio shuttle cart?
ApexDrive shuttle carts use heavy-duty Lithium Iron Phosphate (LiFePO4) battery packs designed for deep-cycle industrial performance. A fully charged battery pack delivers 8 to 10 hours of continuous operating time. With our fast-charging station, a full recharge takes approximately 3 hours. Batteries are rated for over 2,000 charge cycles before capacity degrades to 80%, providing a typical operational service life of 5 to 7 years under standard shift operations.
3. How does the automated shuttle system perform in sub-zero cold storage facilities?
Our cold-chain automated pallet shuttles are specifically built for freezing environments down to -25°C (-13°F). They feature internal electric heating elements for control circuit boards, low-temperature synthetic lubricants, condensation-proof sensor optics, and cold-optimized battery chemistry. This prevents battery capacity loss and mechanical freezing during continuous cold room operation.
4. What safety mechanisms are built into the shuttle cart to prevent collisions or drops?
Safety is built into every layer of our hardware design. Each shuttle cart features front and rear laser obstruction detection sensors that stop movement automatically if an obstacle or misaligned pallet is detected. Additional safety features include end-of-rail mechanical stoppers, anti-tilt sensor arrays, emergency stop buttons, and optical edge detection that prevents the shuttle from driving off the end of an open rail channel.
5. How are spare parts handled for international export projects?
We supply a recommended spare parts package with every international order, including replacement sensors, drive belts, remote controllers, and wheel assemblies. Standard electrical components utilize globally recognized brands (such as Schneider, Siemens, and Omron), allowing local procurement if needed. Additionally, express air shipments of factory original parts are dispatched within 24 hours of request.
6. What steel standards and quality certifications do your racking systems meet?
ApexDrive racking systems are designed and manufactured in compliance with international structural racking standards, including European EN 15512 standards and RMI (Rack Manufacturers Institute) specifications. Our production facility is certified under ISO 9001:2015 for quality management, and our structural equipment carries full CE certification for European compliance.