ApexDriveRACKING
Engineered Cold Storage Pallet Racking Systems
Precision-manufactured structural steel racks, teardrop beam systems, portable stacking frames, and shuttle storage components designed specifically for sub-zero freezer environments.
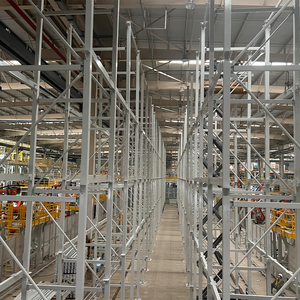
Neat Arrangement 5 Layer Steel Pallet Supported Goods Storage Frame for Cold Chain Base Warehouse Pallet Rack
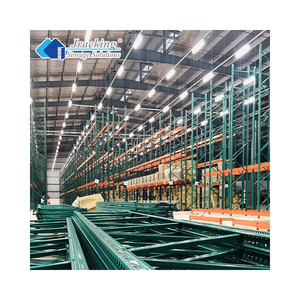
Jracking Heavy Duty Warehouse Racks Shelves RMI Certified Steel Teardrop Pallet Racking For Cold Storage Warehouse
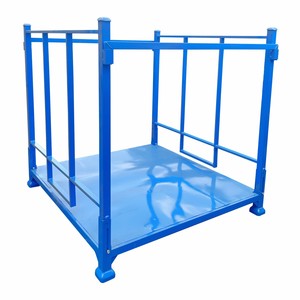
Manufacturer Custom Portable Stacking Racks with Steel Pallet Base & Removable Corner Posts for Cold Chain Logistics
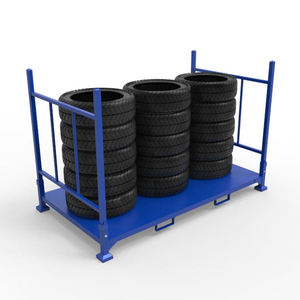
Factory Direct Sales Stack And Rack Stacking Up Racks Heavy Duty Stackable Iron Steel Pallets For Cold Storage
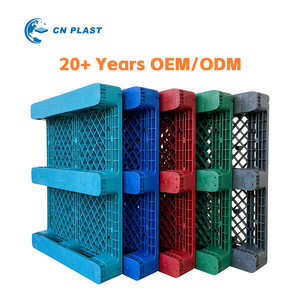
CNPLAST Model 1210 HDPE Rackable Plastic Pallet 1200x1000mm Heavy Duty 4-Way Entry for Industrial Transportation Cold Chain
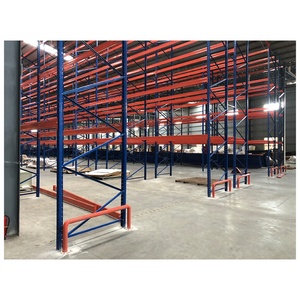
Heavy Duty Steel Cold Chain Selective Pallet Storage Rack
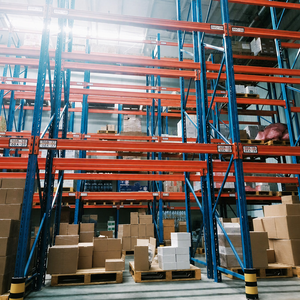
Steel Pallet Logistics Warehouse Storage Rack Heavy Duty Adjustable Selective Pallet Racking for Cold Chain
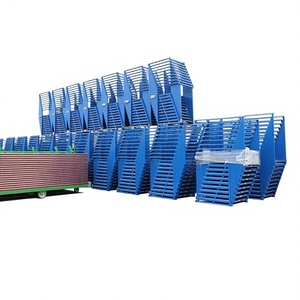
Wholesale Blue Steel Cold Storage Pallet Racking Large-scale Freezer Warehouse Stacking Racks Food Cold Chain Warehouse Turnover
Cold Chain Storage Infrastructure: OEM Engineering & Strategic Design White Paper
Operating a cold storage facility is an exercise in managing extreme thermal dynamics and escalating operational expenditure. Unlike ambient warehousing—where floor space is the primary financial metric—cold storage costs are dominated by the continuous volumetric refrigeration of insulated rooms. Every cubic meter of unused air represents wasted electricity, increased compressor wear, and diminished operational margins. Consequently, selecting a Custom OEM Cold Chain Pallet Racking Supplier is not merely an equipment procurement transaction; it is a critical structural and thermodynamic engineering decision that directly impacts facility profitability for decades.
Information Gain Insight: Structural steel exposed to continuous temperatures between -18°C and -40°C undergoes microstructural changes. Standard carbon steels experience embrittlement when subjected to cyclic thermal stress, leading to premature fatigue failure under heavy static and dynamic loads. Certified OEM suppliers must specify low-alloy high-strength structural grades (such as Q355E or equivalent ASTM grade steels) verified by Charpy V-notch impact testing at -40°C.
This technical guide evaluates the metallurgical parameters, storage density configurations, automation integration paths, and OEM supplier verification methodologies required for modern cold storage infrastructure. Whether configuring deep-lane semi-automated pallet shuttles or heavy-duty teardrop selective frameworks, understanding the physical interaction between steel chemical composition, surface finish, and low-temperature stress propagation is essential for engineering compliance and operational safety.
Sub-Zero Metallurgy: Ductile-to-Brittle Transition & Anti-Corrosion Protection
Cold room structural safety depends on how steel handles mechanical stress below freezing points. As ambient temperature drops, conventional carbon steel (such as standard Q235B) experiences a reduction in impact toughness. This critical boundary—known as the Ductile-to-Brittle Transition Temperature (DBTT)—marks the point where steel transitions from absorbing plastic deformation to experiencing sudden catastrophic brittle fracture without prior warning deformation.
Micro-Alloyed Steel Selection
For sub-zero storage (-20°C to -40°C), structural components are roll-formed from micro-alloyed steel grades (Q355D/E) with controlled carbon equivalents, elevated manganese ratios, and trace vanadium or niobium additives to guarantee high impact energy absorption at sub-zero levels.
Charpy V-Notch Verification
OEM material batches undergo rigorous Charpy V-Notch impact testing to measure energy absorption (Joules) at -40°C. Upright columns and load beams must exhibit minimum impact toughness thresholds to withstand sudden impact forces from forklifts in freezing conditions.
Dual-Finish Coating Systems
Condensation during freeze-thaw cycles drives surface corrosion. We utilize hot-dip galvanizing (HDG) conforming to ISO 1461 (80-100 µm zinc coating) or a 220-meter automated line applying thermosetting epoxy-polyester powder cured at 180°C to prevent micro-fissure flaking.
Surface Protection Comparison: Powder Coating vs. Hot-Dip Galvanizing (HDG)
When selecting surface treatments for cold chain racking, project engineers must weigh ambient humidity, wash-down chemicals, and mechanical impact. The following data visualization matrix outlines the operational envelope for each surface treatment option:
| Coating Specification | Layer Thickness | Optimal Temperature Range | Condensation & Humidity Resistance | Typical Application Environment |
|---|---|---|---|---|
| Electrostatic Powder Coating | 60 – 80 microns (µm) | -15°C to +50°C | Moderate (Requires climate control) | Chilled distribution centers, standard pallet racks, order picking zones |
| Thermosetting Epoxy-Polyester | 80 – 110 microns (µm) | -25°C to +40°C | High (Sealed resin barrier) | Blast freezers, sealed food storage rooms, cold turnover facilities |
| Hot-Dip Galvanizing (HDG) | 80 – 120+ microns (µm) | -40°C to +60°C | Maximum (Metallurgical zinc-iron bond) | Deep freeze (-30°C), high humidity, seafood wash-down, outdoor docks |
High-Density System Architecture & Cold Storage Cubic Optimization
Maximizing storage density while maintaining throughput speed is the core objective of cold chain storage layout design. Traditional selective pallet racking offers 100% direct accessibility but requires wide aisles that consume up to 60% of total cold room footprint. To optimize thermal efficiency, modern freezer facilities employ high-density structural systems customized to specific stock-keeping unit (SKU) profiles and stock rotation rules (FIFO vs. LIFO).
Comparative Analysis of Cold Chain Storage Racking Technologies
| Storage System Type | Volumetric Density | Direct Accessibility | Cold Room Energy Savings | Stock Rotation Rule | Recommended Cargo Profile |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Direct Access | Baseline (Low) | FIFO / LIFO Flexible | High SKU variety, fast turnover, low volume per SKU |
| Drive-In / Drive-Thru Racking | 65% – 75% | Low (Per Lane) | High (+25% vs Selective) | LIFO (Drive-In) / FIFO (Drive-Thru) | Seasonal produce, batch agricultural goods, single-item bulk |
| Radio Shuttle Racking | 80% – 88% | Semi-Automated (Per Lane) | Very High (+35% vs Selective) | FIFO or LIFO Selectable | Frozen meats, dairy, ice cream, high-volume fast-moving consumer goods |
| Very Narrow Aisle (VNA) | 60% – 70% | 100% Direct Access | Moderate (+15% vs Selective) | FIFO / LIFO Flexible | Pharmaceuticals, medical cold chain, high-density order picking |
| Automated AS/RS Stacker Crane | 88% – 95% | 100% Automated Access | Maximum (+50% vs Selective) | Software-Driven FIFO | Mega-scale distribution hubs, automated dark warehouses (-25°C) |
Energy Reduction Formula: By transitioning from standard Selective Racking to a Radio Shuttle System or Automated AS/RS, cold room floor area can be reduced by up to 45% for the same pallet capacity. This reduction translates to a direct 30-40% drop in continuous compressor cooling loads, delivering full capital expenditure payback within 24 to 36 months of deployment.
Future Procurement & Technological Trends in Cold Chain Logistics
The global cold chain industry is undergoing a structural shift driven by stringent food safety regulations, pharmaceutical distribution demands, energy cost volatility, and widespread labor shortages in sub-zero environments. OEM procurement strategies are evolving from simple steel purchasing toward integrated, automated, and energy-optimized storage systems.
Ultra-Low Temperature Shuttle Automation
Modern radio shuttle systems are equipped with specialized low-temperature lithium-iron-phosphate (LFP) batteries featuring internal thermal management systems, enabling continuous operation down to -30°C without capacity degradation or battery voltage drop.
Modular OEM Customization & Standardized Kits
Global buyers are moving away from proprietary, locked-in designs. Procurement preference is shifting toward standard RMI and FEM compliant teardrop and upright profile geometry, allowing seamless replacement, expanding modular frames, and integrating third-party WMS hardware.
IoT Stress Sensors & Digital Twin Monitoring
High-bay freezer racks are increasingly specified with integrated strain gauges and tilt sensors. Connected to warehouse digital twins, these sensors monitor real-time beam deflection, thermal expansion forces, and structural impact loading from material handling equipment.
OEM Enterprise Capabilities: Full-Process Manufacturing Control
As an established industrial racking manufacturer founded in Nanjing, China, our manufacturing operations operate under strict ISO 9001:2015 Quality Management and CE Certification standards. Our state-of-the-art 20,000 square meter production facility is specifically engineered for high-precision, structural-grade warehouse storage system fabrication.
In-House Production & Quality Control Pipeline
From raw steel coils to loaded export containers, every manufacturing step is conducted under controlled in-house procedures to guarantee component consistency, dimensional tolerance, and structural performance under freezing conditions:
1. Sourcing Certified Raw Steel
Coils are sourced directly from tier-1 steel mills including Baosteel, Masteel, and Wuhan Iron and Steel. Mill test certificates accompany every batch, verifying exact chemical analysis, yield strength, and tensile limits for Q235B and Q355B/E grades.
2. High-Precision Cold Roll Forming
Continuous German-technology roll forming machines roll upright posts up to 12 meters in length without mid-welds. Cumulative hole-pitch tolerance is held within ±2 mm over 12 meters, ensuring smooth beam locking and precise vertical alignment.
3. Robotic Manipulator Welding
Heavy-duty beam end connectors, column baseplates, and structural bracing are welded using automated multi-axis robotic welding manipulators. This guarantees full penetration welds, uniform bead geometry, zero porosity, and eliminates human error.
4. 220-Meter Automated Coating Line
Components undergo a 10-stage pre-treatment process including alkaline degreasing, acid rust removal, and ceramic phosphate passivation. Components are then finished on a 220m