ApexDriveRACKING
Direct Factory Catalog
Featured OEM/ODM Industrial Racking Systems
Precision cold-rolled structural steel racking engineered to international standards (EN 15512, FEM 10.2.02, RMI). Browse our core export product lines tailored for high-density distribution centers and automated warehouses.
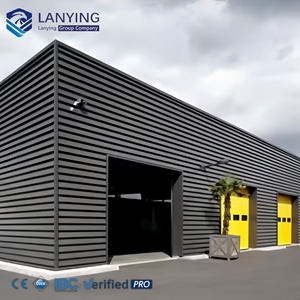
Prefabricated Steel Structure Logistics Warehouse Workshop Industrial Building Commercial Building Steel Structure Warehouse
Contact Us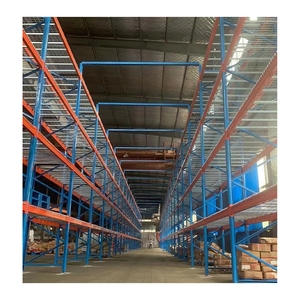
Versatile Storage System Heavy Duty Warehouse Racks Storage Pallet Racking Steel Rack Heavy Duty Pallet Racking By Custom
Contact Us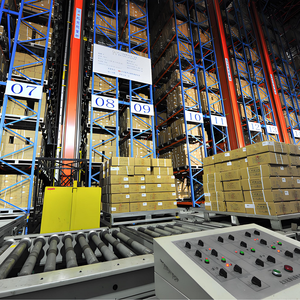
Automatic Double Deep Pallet Racking for High-Capacity Warehouses
Contact Us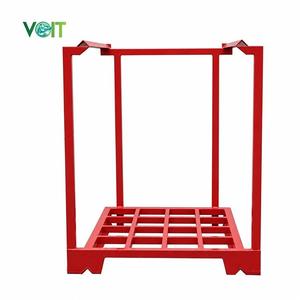
Industrial Storage 1000kg Loading Metal Nestainer Stacking Rack Stacker Pallet
Contact Us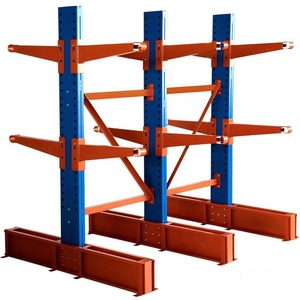
Victory Warehouse Storage Shelving Rack Cantilever Racking Heavy Duty System For Lumber
Contact Us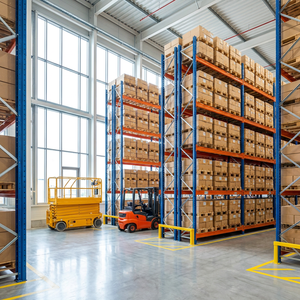
Multi Level Pallet Rack Warehouse Shelving Heavy Duty Shelves Factory Industrial Racking Systems
Contact Us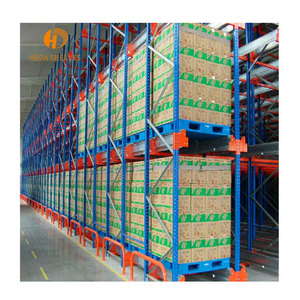
High Density Storage Rack Heavy Duty Drive In Pallet Racking System Design Double Deep Pallet Racks
Contact Us
Double Deep Pallet Rack Heavy Duty Pallet Storage Racking 1000kg/2000kg/3000kg Per Layer Construction Warehouse Storage
Contact Us
White Paper Insight
Navigating Enterprise Racking Procurement: The OEM/ODM Engineering Edge
In modern global supply chain infrastructure, warehouse rack procurement has transitioned from buying standard off-the-shelf steel hardware to executing highly engineered structural integration projects. As premier OEM/ODM Pallet Racking Suppliers & Exporters, we specialize in bridging the gap between complex building acoustics, floor slab capacity constraints, automated material handling technology, and optimized pallet position yield.
Standard warehouse setups frequently suffer from dead aisle space, unoptimized beam height intervals, and seismic safety vulnerability under maximum payload stress. Through rigorous structural analysis using Finite Element Analysis (FEA) software, our engineering team custom-designs upright cold-formed profile geometries (utilizing high-grade Q235B and Q355B structural steel sourced directly from Baosteel and Masteel) to ensure structural safety factors exceeding 1.8 while keeping material displacement within strict L/300 deflection metrics.
20,000+
Sqm Manufacturing Base
30,000T
Annual Steel Processing
6,000+
Global Projects Delivered
150+
Advanced Machinery Sets
Manufacturing Excellence
Why Global Enterprise Brands Partner With Us
Fully integrated in-house manufacturing, rigorous raw material selection, and verified structural certification eliminate supply chain risk for overseas contractors and system integrators.
Traceable Raw Materials
We source cold-rolled structural coil steel exclusively from premier Chinese state-owned steel mills including Baosteel, Masteel, and Wuhan Iron and Steel. Complete chemical composition analysis and physical tension mill certificates (Q235B / Q355B) accompany every production batch.
Precision Roll Forming
Operating dedicated automated continuous roll-forming lines utilizing German technology, our upright punch profiles maintain a cumulative hole-pitch error under ±2 mm over a 12-meter single vertical continuous length, guaranteeing exact beam connector locking engagement.
Robotic Welding Rigidity
Beam end connectors (3-hook to 5-hook heavy duty claws) are joined using multi-axis automatic robotic manipulator welding stations. Full-penetration continuous weld seams eliminate porosity and prevent beam rotation under dynamic fork truck loading.
220m Swiss Gema Coating Line
Components undergo 10-stage chemical degreasing, acid rust removal, and silane pre-treatment before receiving thermosetting polyester powder coating via Swiss Gema electrostatic guns, cured at 180°C for exceptional impact and salt-spray resistance.
Pre-Shipment Trial Assembly
To ensure zero site-assembly delays for international buyers, high-bay structural upright frames, mezzanine beams, and shuttle guide rails undergo trial module assembly inside our factory prior to container packing and export clearance.
Export-Grade Heavy Strapping
Uprights and beam bundles are wrapped in protective polyethylene films, reinforced with corner edge protectors, and secured with multi-tier heavy steel strapping on custom plywood skids designed for safe forklift container unloading.
Technical Selection Matrix
Industrial Racking System Performance Comparison
Selecting the optimum pallet rack system requires balancing floor space density against individual pallet accessibility and handling speed. Review our comprehensive engineering evaluation below.
| Racking Architecture | Storage Density Rating | Pallet Direct Accessibility | Forklift Operating Requirements | Ideal Application Scenario | Relative Cost / Pallet |
|---|---|---|---|---|---|
| Selective Pallet Racking | Medium (40-50% Floor Util.) | 100% Direct Selective Access | Standard Counterbalance / Reach Truck | High SKU variety, fast stock turnover, FMCG hub | Economical Base Level |
| Double Deep Pallet Racking | High (55-65% Floor Util.) | 50% Direct Access (FILO per deep pair) | Specialized Pantograph / Deep Reach Truck | Identical SKU batching, medium turnover rate | Moderate Low |
| Drive-In / Drive-Thru Racking | Very High (65-75% Floor Util.) | Low (LIFO / FIFO lane selective) | Standard Forklift enters internal rack bay | Bulk homogenised inventory, seasonal cold storage | Moderate |
| Radio Shuttle Cart Racking | Ultra High (75-85% Floor Util.) | High Speed FIFO/LIFO per Lane | Standard Forklift + Battery Powered Shuttle Cart | Cold chain logistics (-25°C), high-volume food & beverage | Moderate High (High ROI) |
| VNA (Very Narrow Aisle) Racking | Very High (60-70% Floor Util.) | 100% Direct Selective Access | VNA Turret Truck guided by Wire/Rail System | Tall clear-height facilities (10m-15m), high SKU density | Moderate High |
| AS/RS Automated Racking | Maximum (85-95% Height Util.) | Fully Automated 24/7 WMS Control | Automated Stacker Crane / Shuttle Conveyor | Smart factories, dark warehousing, high-labor cost regions | Capital Intensive (Max Efficiency) |
2025–2030 Strategic Roadmap
Future Procurement & Technology Evolution Trends
Warehouse storage infrastructure is undergoing rapid technological convergence. Procurement directors must account for five structural macro-trends to avoid premature system obsolescence.
1. Hybrid AMR/AGV Racking Integration
Traditional static pallet racks are being redesigned with specialized low-level base clearance, high-precision guide rails, and reflective optical sensors to accommodate Autonomous Mobile Robots (AMRs) and Automated Guided Vehicles (AGVs). Future-proof racking requires engineered beam tolerances that support robotic picking arms without physical human intervention.
2. Advanced Anti-Corrosion Materials for Cold Chain
With global demand for fresh food cold chains spiking, traditional liquid paint coatings fail due to micro-cracking in sub-zero environments. Procurement is shifting rapidly toward hot-dip galvanizing (HDG according to EN ISO 1461) and pre-galvanized Zinc-Aluminum-Magnesium (ZAM) structural steel profiles that offer self-healing edge corrosion protection in humid or freezing temperatures.
3. Sensorized Smart Racking (IoT Structural Monitoring)
Large distribution hubs are embedding strain gauges, inclination sensors, and collision-warning beacons directly into upright columns. Connected to cloud-based warehouse analytics platforms, these smart racking components provide real-time alerts for dangerous fork truck impacts, frame deflection overloads, and seismic stress detection, dramatically reducing catastrophic rack collapses.
4. Modular & Demountable Racking Infrastructure
Logistics operators operating under short-term commercial warehouse leases demand modular, bolt-together racking structures. High-strength 8.8-grade bolted upright frame assemblies allow fast dismantling, reconfiguration, and height expansion without structural field welding or scrap metal loss when facilities relocate.
6-Step Quality Control Protocol
How We Guarantee Structural Reliability on Global Shipments
Every piece of steel processed in our 20,000 m² factory follows strict quality control checkpoints verified under ISO 9001:2015 and CE certification standards.
01
Chemical & Physical Steel Testing
Raw steel coils undergo ultrasonic thickness inspection and yield stress tensile testing before entering cold roll-forming lines.
02
Laser-Guided Hole Punching
Automated punching dies produce teardrop, diamond, or 75mm-pitch column holes with zero burr and exact vertical alignment.
03
Robotic Seam Welding
Box beams and step beams are welded to connector claws via robotic manipulators with continuous, non-porous weld seams.
04
Automated Pre-Treatment & Powder Spray
A 220-meter automated powder coating line applies Swiss Gema electrostatic powder coat, cured at 180°C for max durability.
05
Load Bearing Deflection Test
Randomly selected beam spans are subjected to 1.5x nominal payload testing to measure structural elastic return and deflection.
06
Export Container Loading Control
Plywood skid packing, heavy steel banding, and wrapped corner guards prevent ocean freight shipping abrasion and moisture ingress.
Procurement Knowledge Base
Frequently Asked Questions by International Buyers
Technical, logistical, and commercial answers to help procurement managers and engineering contractors plan racking projects effectively.
Q What critical facility information is required to produce a CAD layout design and quotation?
To generate a precise engineering drawing and static load report, we require: (1) Architectural CAD drawing of the building showing clear undersides of truss heights, column spacing grids, dock door locations, and fire sprinkler clearances; (2) Pallet unit load specs including width, depth, overall height (including pallet base), and gross weight per pallet; (3) Number of unique SKUs and total storage pallet positions required; (4) Forklift specifications (minimum aisle turning radius, maximum mast lift height); and (5) Inventory management strategy (FIFO or LIFO stock flow).
Q Which steel grades and surface treatment processes are standard across your manufacturing lines?
We primary roll-form structural members from Q235B and Q355B structural coil steel supplied by top-tier mills (Baosteel and Masteel). Components go through a 10-stage chemical pre-treatment process (degreasing, rust removal, surface conditioning, and silane coating) followed by electrostatic powder coating using Swiss Gema technology, baked at 180°C. For humid, cold storage, or outdoor applications, hot-dip galvanizing according to EN ISO 1461 is available.
Q How do you support site installation and assembly for international buyers outside of China?
Every exported racking project includes detailed 3D assembly drawings, column anchoring installation guides, and English instruction manuals. Our engineering team provides 24/7 remote video consultation during assembly. For large-scale logistics centers or automated AS/RS high-bay installations, we can dispatch certified installation supervisors and mechanical crews to lead on-site construction.
Q What safety compliance standards and structural certifications do your racking systems meet?
Our storage racking systems are engineered in accordance with European FEM 10.2.02 and EN 15512 specifications, American RMI (Rack Manufacturers Institute) standards, and Australian AS 4084-2012 codes. The factory operates under ISO 9001:2015 Quality Management System certification and holds official CE mark compliance for structural steel products.
Q How are components packaged to prevent damage during long-distance ocean transport?
Upright frames and horizontal beams are bundled using multi-layer protective film and plastic edge caps, bound by heavy-duty steel strapping onto custom wood skids. Accessories (baseplates, safety pins, row spacers, expansion bolts, and levelling shims) are packed into heavy-duty corrugated cartons anchored to fumigated plywood pallets, facilitating quick customs inspection and container offloading.
Start Your Engineering Plan
Optimize Your Warehouse Storage Density Today
Contact our senior storage engineering team to receive a free, no-obligation CAD layout proposal, FEA load calculation, and factory-direct price quotation within 24 hours.
Contact Us