ApexDriveRACKING
Featured Product Lineup
Heavy-Duty & Custom Pallet Racking Systems
Explore our top-tier export-grade racking configurations, custom roll-formed from high-yield Q235B/Q355B steel to deliver safety factors up to 1.85 and maximum vertical space efficiency.
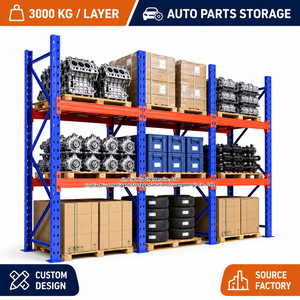 Selective
200-4000KG Selective Pallet Racking Heavy Duty Warehouse Rack Custom Size OEM Manufacturer
Cap: 200-4000kg/Beam
Q235B / Q355B
100% Access
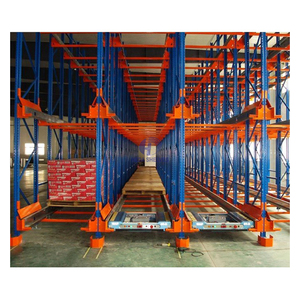 High Density
Customized Used High Quality Steel Heavy Duty Automatic Storage System Shuttle Pallet Rack for Warehouse
Radio Shuttle
FIFO / LIFO
Cold Storage Ready
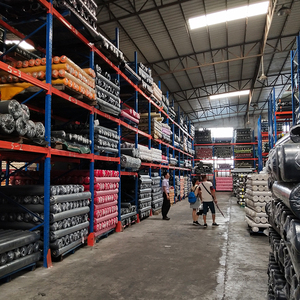 Free Design
Highly Customizable Free Design Storage Rack for Various Heavy Duty Storing 1000KG 2000KG 3000KG Pounds Tons
1000-3000kg/Level
CAD Layout
OEM Custom
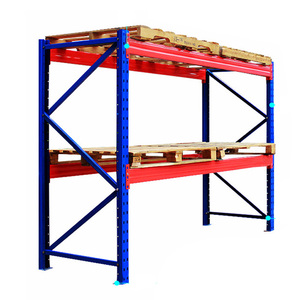 Weatherproof
Outdoor Pallet Racking Metal Storage Organizer Rack For Warehouse Store Factory 1000KG 2000KG 3000KG Pounds Tons
Hot-Dip Galvanized
Anti-Corrosion
Outdoor Duty
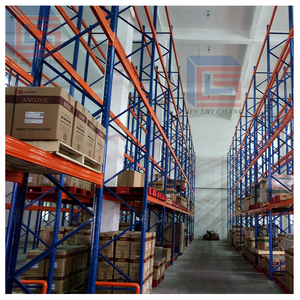 Industrial
Heavy Duty Selective Pallet Rack Steel Warehouse Storage Racking System for Industrial Logistics and Customized Use
Logistics Grade
Adjustable Beam
Safety Pins Included
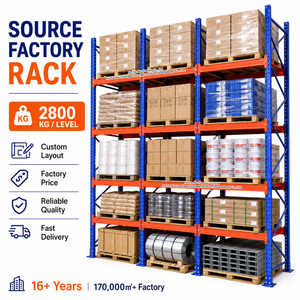 High Bay
2800KG 5 Levels High Bay Industrial Pallet Racking Heavy Duty Warehouse Rack System
2800kg Rating
5 Tier Vertical
Max Volume
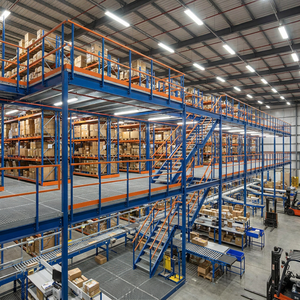 Custom OEM
Customized Industrial Pallet Rack System Warehouse Storage Solution Manufacturer
Engineered Solution
Baosteel Raw Material
Turnkey Engineering
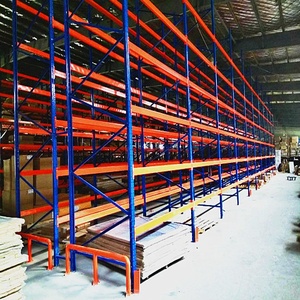 CE & ISO
ISO9001 CE Euro Standard Outdoor Pallet Rack Storage Racking System Adjustable
CE Certified
Euro Standard
Pitch 50mm/75mm
20,000 m²
Modern Manufacturing Base
30,000+ Tons
Annual Steel Processing Capacity
6,000+
Global Projects Installed
150+ Sets
Precision Roll-Forming & Robotic Equipment
Executive Technical White Paper
Engineering Excellence & Structural Mechanics in Custom Pallet Racking Systems
In modern industrial logistics and material handling operations, warehouse space optimization is no longer just a structural requirement—it is a critical driver of supply chain agility and operational ROI. Selecting a custom pallet racking system requires deep engineering evaluation regarding load-bearing capacity, column buckling strength, horizontal sway stability, structural steel grade selection, and seismic resilience. As a leading manufacturer and exporter, ApexDrive Industrial Racking Co., Ltd. builds structural systems engineered strictly in compliance with international standards, including FEM 10.2.02 (European Design Code for Static Steel Pallet Racking) and RMI (Rack Manufacturers Institute ANSI MH16.1).
The structural integrity of a custom pallet rack originates from raw material selection. ApexDrive utilizes structural steel coils sourced exclusively from tier-1 steel producers such as Baosteel, Masteel, and Wuhan Iron & Steel. Components are roll-formed from cold-rolled Q235B steel (nominal yield strength of 235 MPa) or high-yield Q355B structural steel (nominal yield strength of 355 MPa). By leveraging Q355B steel for high-bay upright frames and heavy-load beam spans, we achieve a superior strength-to-weight ratio while maintaining structural safety factors exceeding 1.80 under maximum rated payload conditions.
Mechanical Analysis: Roll-Formed Upright Profiles & Beam Deflection Limits
The vertical upright frame is designed to resist combined axial compression and bending moments induced by eccentric loading and frame displacement. Upright profiles range from 80mm to 120mm face widths with wall thicknesses from 1.8mm to 2.5mm. Precision cold roll-forming ensures hole-pitch cumulative tolerance remains under ±2 mm over a continuous 12-meter upright length. This tight mechanical tolerance is essential to guarantee that beam connector hooks seat tightly, eliminating structural slop and dynamic sway under heavy forklift operations.
Horizontal load beams are fabricated as interlocking box-beam sections composed of two C-profiles nested and robotically seam-welded. According to FEM specifications, beam deflection under full static payload must not exceed L/200 (where L is the clear beam length) and preferably remains within L/300 for automated and high-bay operations. ApexDrive box beams incorporate automatic spring-lock safety pins that prevent accidental beam dislodgement caused by upward forklift impacts, ensuring worker safety and operational compliance.
Certified Q355B Steel
Mill-certified high-yield steel coils delivering maximum buckling resistance and extended fatigue life under dynamic cyclical loads.
Swiss Gema Powder Line
220-meter continuous electrostatic coating line operating at 180°C curing temperature for maximum corrosion and scratch protection.
Seismic M7 Engineering
Engineered baseplates, heavy-duty floor anchor bolts, and frame bracings calculated to withstand magnitude 7 earthquake accelerations.
Technical Comparison: Steel Storage Racking Architectural Configurations
Choosing the optimal custom pallet racking framework depends on key operational parameters: Stock Keeping Unit (SKU) diversity, inventory turnover speed, floor area availability, ceiling height clearance, and handling equipment capabilities. The following engineering matrix summarizes performance metrics across high-density storage configurations manufactured by ApexDrive.
| Racking Architecture | Storage Density | Pallet Access (Selectivity) | Handling Equipment Required | Ideal Application Sector | Typical Max Bay Load |
|---|---|---|---|---|---|
| Selective Pallet Racking | Medium (40-50%) | 100% Direct Access | Counterbalance / Reach Truck | 3PL FMCG, General Logistics, Mixed SKUs | Up to 24,000 kg / Frame |
| Radio Shuttle Racking | Ultra-High (80-90%) | Deep-Lane (FIFO / LIFO) | Standard Forklift + Battery Shuttle | Cold Storage, Food & Beverage, Bulk Goods | Up to 1,500 kg / Pallet |
| VNA (Very Narrow Aisle) | High (65-75%) | 100% Direct Access | VNA Turret Truck / Articulated Forklift | High-Bay Distribution Centers, E-Commerce | Up to 20,000 kg / Frame |
| Drive-In / Drive-Through | High (70-80%) | LIFO / FIFO Lane-Based | Standard Forklift (Enters Rack Lane) | Seasonal Staging, Few SKUs Bulk Volume | Up to 15,000 kg / Lane |
| AS/RS Automated High-Bay | Maximum (90%+) | Fully Automated Access | Stacker Cranes / WMS Controlled Conveyors | Smart Factories, Automated Distribution Hubs | Height up to 40+ Meters |
Global Procurement Trends & Industry Evolution (2025–2030)
The international material handling landscape is experiencing a structural migration toward semi-automated and automated warehousing solutions. Major warehouse operators, logistics integrators, and industrial manufacturing plants are prioritizing structural storage systems that natively integrate with Autonomous Mobile Robots (AMRs), Automated Guided Vehicles (AGVs), and Warehouse Management Systems (WMS).
Key technological trajectories shaping custom pallet racking procurement include:
1. Hybrid Radio Shuttle & AGV Integration: Traditional drive-in racks are rapidly being superseded by self-powered radio shuttle racking systems. Modern radio shuttles are equipped with laser distance sensors, Wi-Fi 6 communication modules, and lithium iron phosphate (LiFePO4) battery packs capable of operating seamlessly in cold storage environments down to -25°C. When combined with AGVs for main-aisle transfer, warehouses achieve end-to-end automated material handling with zero human intervention.
2. Sustainable Surface Finishes & Hot-Dip Galvanizing Demand: Environmental protection standards and harsh operating environments have heightened buyer requirements for structural durability. For outdoor pallet racking and cold-chain facilities exposed to condensation, hot-dip galvanizing (HDG) compliant with ISO 1461 provides a zinc coating thickness of 65-85 μm, delivering corrosion resistance exceeding 20 years. Indoor systems utilize zero-VOC electrostatic polyester powder coating, eliminating toxic off-gassing while preserving surface hardness.
3. Modular Mezzanine & Multi-Tier Rack Platforms: As urban industrial land costs rise globally, warehouse operators are leveraging clear ceiling heights by building rack-supported mezzanines and heavy-duty structural steel platforms. These systems convert vertical volume into multi-level order picking floors, doubling or tripling effective square footage without incurring building expansion costs.
Why Partner With ApexDrive
Factory Direct Manufacturing Strength & Quality Guarantee
From structural engineering analysis to automated roll-forming and overseas installation support, ApexDrive delivers end-to-end supply chain reliability.
Integrated Manufacturing Plant
Our 20,000 m² modern manufacturing facility in Nanjing, China houses 150+ sets of automatic roll-forming lines, robotic welding manipulators, and high-speed punching presses, producing over 30,000 tons of structural steel racking per year.
Strict ISO 9001 & CE Compliance
Every batch of steel components undergoes pre-shipment trial assembly, dimensional accuracy verification, weld flaw detection, and coating thickness testing. Certified under ISO 9001:2015 and CE standards for European compliance.
Free Engineering CAD & 3D Design
Our structural engineers provide free layout design, 3D building modeling, structural load calculation reports, and seismic evaluation tailored precisely to your building CAD drawing and forklift specifications.
Export-Safe Container Packing & Global Dispatch
Uprights and beams are bundled with multi-tier steel strapping and corner protective wraps. Small hardware is packed on solid plywood pallets to ensure damage-free transit across sea freight containers.
Procurement FAQ
Frequently Asked Questions by International Buyers
Clear engineering insights to assist procurement managers, warehouse operators, and system integrators during project evaluation.
What essential parameters are required to generate a custom warehouse racking layout?
To provide an optimized engineering layout and load calculation report, we require: (1) Warehouse building CAD drawings or dimensions detailing clear height, column grid locations, doors, and sprinkler clearance; (2) Pallet unit load specification: length x width x overall height (including goods) and maximum weight per pallet; (3) Required storage capacity and SKU count; (4) Forklift truck details: model, aisle width requirement, maximum lift height, and turning radius; (5) Material flow logic: FIFO (First-In, First-Out) or LIFO (Last-In, First-Out).
How do Q235B and Q355B steel grades differ in heavy-duty racking applications?
Q235B steel provides a nominal yield strength of 235 MPa and is the standard material for standard selective pallet racking beams and medium-load upright frames. Q355B structural steel provides a higher yield strength of 355 MPa (approx. 50% stronger in yield). Utilizing Q355B steel allows us to engineer high-bay upright frames, heavy-duty beam spans, and heavy mezzanine columns with reduced steel thickness while achieving equivalent or superior safety factors, optimizing shipping weight and load rating.
What surface protection finish is recommended for cold storage or outdoor racking?
For indoor ambient warehouses, our 220-meter automatic electrostatic powder coating line applies a high-durability epoxy/polyester coating (60-80 μm thickness) cured at 180°C. For sub-zero cold storage facilities with high humidity condensation or outdoor metal storage racks, we strongly recommend Hot-Dip Galvanizing (HDG) compliant with ISO 1461. Hot-dip galvanizing submerges the fabricated steel into molten zinc, forming a metallurgical alloy coating that completely seals internal structural tubes and exterior edges against rust for over 20 years.
How does ApexDrive support overseas racking installation and technical assembly?
Every export container ships with comprehensive English installation manuals, step-by-step CAD assembly drawings, and structural component packing lists. We provide remote 24/7 video technical support to your local installation team. For large-scale automated high-bay warehouses, AS/RS projects, or extensive mezzanine platforms, ApexDrive can dispatch experienced installation supervisors and project engineers directly to your overseas job site to manage full erection, alignment, and load testing.
What structural safety standards and certifications do your racking systems comply with?
ApexDrive custom racking systems are engineered and tested in strict accordance with European FEM 10.2.02 standard specifications, ISO 9001:2015 Quality Management Systems, and European CE certification standards. Structural calculations account for static load capacity, dynamic impact factors, beam deflection limits (L/200 to L/300), horizontal sway displacement, and local seismic zone acceleration requirements.