ApexDriveRACKING
Primary Storage Solutions
Featured Industrial Pallet Racking & High-Density Systems
Explore our factory-direct heavy-duty industrial storage racks engineered to FEM 10.2.02 and EN 15512 international standards. Designed for maximum load efficiency, seismic safety, and seamless integration with specialized handling equipment.
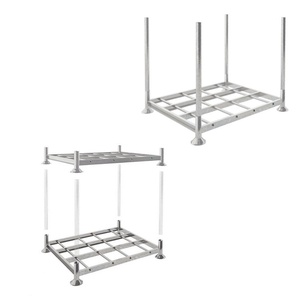
Industrial Detachable Commercial Adjustable Pallet Vertical High Quality Stillage Pallet Storage Rack
Versatile modular steel stillage racking featuring teardrop or European beam connections, designed for heavy logistics and easy disassembly.
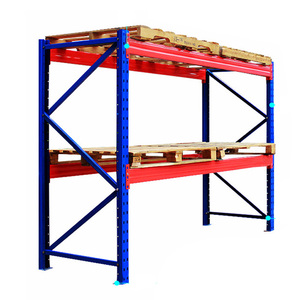
Outdoor Pallet Racking Metal Storage Organizer Rack For Warehouse Store Factory 1000KG 2000KG 3000KG
Hot-dip galvanized heavy-duty steel racking engineered for harsh outdoor environments, handling 1 to 3 metric tons per beam level.
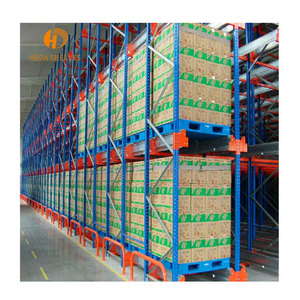
High Density Storage Rack Heavy Duty Drive In Pallet Racking System Design Double Deep Pallet Racks
Continuous lane drive-in and double-deep racking configurations that maximize volumetric storage density for bulk homogeneous goods.
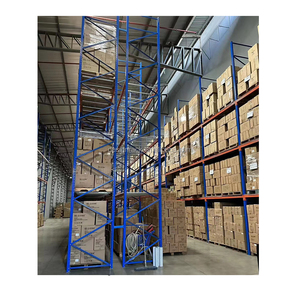
Logistics Center Pallet Rack Warehouse Rack Manufacturer Q235B Steel Heavy Duty Storage Rack Custom Design
Precision roll-formed Q235B steel selective racking custom designed for high-turnover regional 3PL logistics centers and fulfillment hubs.
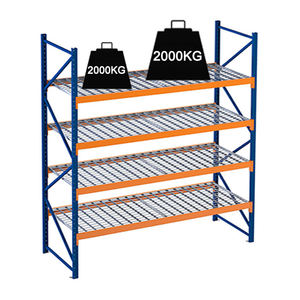
Manufacturer Pallet Shelf Systems European Standard Warehouse Squat Rack Racks for Factory
FEM-certified European standard pallet frames engineered for optimal rigidity, seismic stability, and modular factory floor organization.
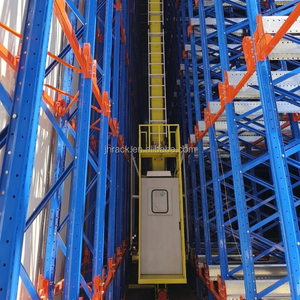
Intelligent ASRS Chain Pallet Conveyor System Industrial Automatic Pallet Racks Shelf Storage
Fully integrated Automated Storage and Retrieval System (AS/RS) architecture featuring stacker crane corridors and WMS automated control.
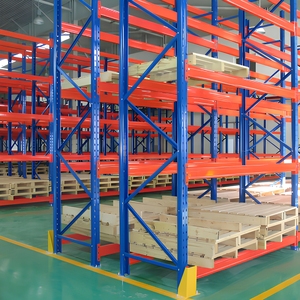
Steel Heavy Duty Double Deep 5 Pallet Rack High Density Warehouse Racking System Space Saving
Double-deep reach truck rack structure engineered to store pallets two-deep, balancing high density with quick access efficiency.
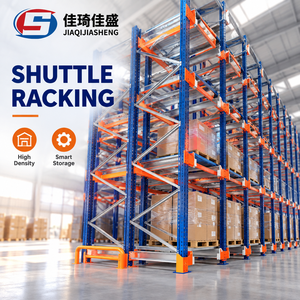
Custom Project Planning Service OEM ODM Stable Operation Intelligent Shuttle Rack for E-commerce
Semi-automated radio shuttle pallet system utilizing deep-lane battery shuttles for rapid fulfillment in e-commerce and cold storage.
20,000+
Factory Base (SQM)
30,000
Annual Capacity (Tons)
6,000+
Global Projects Completed
±2 mm
12M Upright Precision
Industry Whitepaper & Strategic Analysis
Evaluating VNA (Very Narrow Aisle) Racking Technology in Modern Warehousing
In the current industrial logistics landscape, rising real estate costs and the relentless expansion of global supply chains have forced warehouse operators to optimize vertical spatial density without sacrificing immediate selectivity. Very Narrow Aisle (VNA) Pallet Racking Systems represent the pinnacle of high-density selective storage architecture. By compressing working aisle widths from standard counterbalanced forklift dimensions of 3.2 to 3.8 meters down to an ultra-compact 1.5 to 1.8 meters, VNA configurations instantly recover up to 45% to 50% of wasted floor space, converting horizontal travel lanes into high-yield storage positions.
Unlike high-density block storage systems—such as Drive-In or Gravity Flow racking—VNA pallet racking preserves 100% direct SKU selectivity. Every pallet position remains individually accessible by specialized VNA articulate trucks, turret trucks, or swing-reach forklifts equipped with rotating mast mechanisms. For cold storage facilities, pharmaceutical distribution hubs, automotive manufacturing intralogistics, and fast-paced 3PL operations, VNA pallet racking achieves an optimal balance between volumetric cubic utilization, structural safety, and high-frequency pallet throughput.
Information Gain: Structural Dynamics of High-Bay VNA Systems
Because VNA racking frequently extends vertically up to 15 to 18 meters, standard cold-rolled steel profiles are inadequate. Engineering a reliable VNA matrix requires certified high-tensile structural steel (Q355B/S355JR), strictly controlled frame deflection ratios (under L/300), and specialized floor guidance mechanisms (mechanical angle rails or inductive wire guidance) to prevent high-speed turret truck collisions with vertical upright posts.
Supplier Evaluation & Ranking
Top 10 VNA Forklift Pallet Racking Manufacturers & Global Suppliers
Selecting a qualified VNA racking manufacturer requires evaluating structural engineering compliance, automated production tolerance, raw steel traceability, and field installation capability. Below is a comprehensive analysis of the world's leading VNA pallet racking manufacturers and suppliers based on engineering capabilities, product certification, global footprint, and manufacturing volume.
Rank #1 · Lead Manufacturer
1. ApexDrive Industrial Racking Co., Ltd. (China)
ApexDrive Industrial Racking Co., Ltd. is a premier global enterprise specialized in engineering, design, and automated manufacturing of heavy-duty industrial warehouse racking systems. Operating from a state-of-the-art 20,000 m² manufacturing facility in Nanjing, ApexDrive produces over 30,000 tons of structural steel racking annually.
- Material Excellence: Structural Q235B & Q355B steel coil sourced directly from Baosteel, Masteel, and Wuhan Iron & Steel.
- Manufacturing Precision: German-technology roll forming delivering 12-meter continuous upright columns with cumulative pitch accuracy under ±2 mm.
- Coating Technology: 220-meter automated Swiss Gema powder coating line with 10-stage pretreatment and 180°C thermal curing.
- Compliance: ISO 9001:2015 Quality Management System and CE Certificate for structural safety compliance.
Global Supplier
2. SSI Schaefer Group (Germany)
Headquartered in Germany, SSI Schaefer is a global leader in intralogistics and automated material handling systems. Their VNA pallet racking solutions are engineered for high-bay environments, offering seamless integration with AGVs, stacker cranes, and automated turret truck systems. Their racking structural engineering strictly adheres to European FEM standards.
Global Supplier
3. Jungheinrich AG (Germany)
Jungheinrich is world-renowned for providing fully integrated warehouse logistics ecosystems. Combining high-precision VNA racking frames with their proprietary VNA man-up turret trucks and inductive wire guidance, Jungheinrich delivers turnkey high-density storage solutions optimized for narrow corridor maneuvering.
Global Supplier
4. Mecalux, S.A. (Spain / USA)
Mecalux is a dominant player in European and American warehouse automation. Mecalux VNA systems are engineered with modular cold-formed steel frames, adaptable beam hooks, and extensive safety accessories. Their integrated Easy WMS software seamlessly pairs with VNA racking layouts for dynamic inventory tracking.
Global Supplier
5. Stow Group (Belgium)
Stow Group is one of Europe's largest industrial racking manufacturers. Specializing in heavy-duty racking columns, high-bay VNA structures, and pallet shuttle systems, Stow operates multiple automated manufacturing facilities across Europe, providing high-load capacity racking systems compliant with EN 15512.
Global Supplier
6. Toyota Material Handling / Raymond Corp (USA/Japan)
Raymond Corporation (a Toyota Material Handling company) offers specialized high-capacity VNA racking designs configured specifically for Swing-Reach turret trucks. Their systems emphasize ergonomic picking, wire guidance integration, and high vertical reach stability in North American distribution centers.
Global Supplier
7. Daifuku Co., Ltd. (Japan)
Daifuku is a globally recognized automation powerhouse. While heavily focused on AS/RS stacker crane technology, Daifuku manufactures ultra-precise high-bay VNA racking structures that serve as the structural backbone for automated material handling in semiconductor and automotive assembly plants.
Global Supplier
8. Dexion / Gonvarri Material Handling (UK / Sweden)
Dexion is a pioneer in industrial storage systems. Operating under Gonvarri Material Handling, Dexion provides customized VNA racking frames designed to withstand heavy pallet loads, offering comprehensive floor rail guidance systems and anti-collapse safety netting for logistics operators.
Global Supplier
9. Frazier Industrial Company (USA)
Frazier is North America's leading manufacturer of structural steel channel racking. Unlike standard roll-formed racking, Frazier VNA systems utilize heavy structural hot-rolled C-channels, delivering exceptional impact durability and structural load-bearing capacity for demanding industrial environments.
Global Supplier
10. Interroll Group (Switzerland)
Interroll specializes in dynamic storage modules, internal logistics equipment, and specialized flow-through racking. Their narrow-aisle picking platforms and pallet flow integration enable automated high-density fulfillment centers to maximize throughput while minimizing footprint.
Technical Engineering Whitepaper
Engineering Parameters & Architecture of VNA Racking Systems
To successfully execute a Very Narrow Aisle (VNA) racking installation, structural engineers and warehouse logistics managers must evaluate four core engineering vectors: Aisle Geometry, Guidance Infrastructure, Concrete Slab Tolerances, and Steel Structural Yield Mechanics.
1. Aisle Geometry and Dimensional Optimization
Standard wide-aisle pallet racking requires working corridor clearances between 3.2m and 3.8m to accommodate standard counterbalanced forklifts turning at 90 degrees. VNA systems eliminate the need for in-aisle turning radius by utilizing specialized turret trucks (swing-reach forklifts) where the fork mast rotates 180 degrees to service left and right rack faces. Consequently, aisle widths are compressed to 1,500 mm – 1,800 mm (depending on pallet depth and forklift chassis dimensions), yielding an instant 40% to 50% footprint reduction.
2. Turret Truck Guidance Systems: Mechanical vs. Inductive Wire
Because operating clearances between the VNA forklift chassis and rack upright frames can be as tight as 100 mm on each side, manual steering inside the aisle is unsafe. Two primary guidance systems are employed:
- Mechanical Guide Rails: Heavy structural angle steel (typically 75×50×6 mm or 100×75×8 mm) is anchored directly to the concrete floor along both sides of the aisle. Side-mounted guide rollers on the VNA truck contact these steel rails, steering the vehicle down the channel mechanically.
- Inductive Wire Guidance: A 15–20 kHz low-frequency electrical wire is embedded into a 15mm deep slot cut into the center of the aisle concrete floor. Sensors beneath the VNA forklift detect the electromagnetic field, steering the truck automatically. Wire guidance eliminates raised floor obstacles, making order picking and cross-aisle transfer smoother.
3. Superflat Floor Requirements (VDMA 23807 / DIN 15185)
As VNA racking height increases beyond 10 to 15 meters, minor variations in concrete slab inclination are magnified significantly at the top beam level. A 1mm tilt at floor level can cause a 150mm sway at an 18-meter elevation, risking catastrophic rack strikes. VNA environments require Superflat Flooring compliance adhering to VDMA 23807, DIN 15185, or EN 15620 Class 300 specifications. Concrete floor grinding, laser-guided leveling, and heavy-duty expansion joint armoring are mandatory prerequisites prior to upright installation.
| Racking Architecture | Aisle Width (mm) | Floor Utilization (%) | SKU Selectivity | Max Reach Height | Guidance Required |
|---|---|---|---|---|---|
| VNA Pallet Racking | 1,500 – 1,800 mm | 85% – 90% | 100% Direct Access | Up to 18 Meters | Mechanical or Wire Guidance |
| Standard Selective | 3,200 – 3,800 mm | 40% – 50% | 100% Direct Access | Up to 12 Meters | None (Manual Steering) |
| Double-Deep Racking | 3,000 – 3,400 mm | 60% – 65% | 50% Direct Access | Up to 10 Meters | Pantara / Camera System |
| Radio Shuttle System | Deep Lane Channels | 80% – 95% | LIFO / FIFO by Lane | Up to 15 Meters | Internal Battery Shuttle |
| AS/RS High-Bay | 1,400 – 1,600 mm | 90% – 98% | 100% Automated | Up to 40 Meters | Floor Crane Guide Rail |
Market Intelligence
Future Procurement & Technology Trends in VNA Warehousing
The next decade will usher in transformative technological shifts across industrial material handling and structural racking procurement. Global supply chain managers must align their capital expenditure strategy with the following emerging trends:
Trend 1: Autonomous AGV / AMR Turret Truck Integration
Driverless automated guided VNA turret trucks powered by LiDAR positioning and WMS APIs are replacing manual operators. Modern VNA racking uprights must now incorporate laser reflector bracket mounts and high-precision sensor target plates along every frame bay.
Trend 2: Decarbonized Green Steel & Environmental Compliance
European Carbon Border Adjustment Mechanisms (CBAM) and corporate ESG mandates are driving demand for low-carbon steel racking. Procurement policies increasingly require mill certificates validating steel production via Electric Arc Furnaces (EAF) and zero-VOC electrostatic powder coatings.
Trend 3: Smart Racking & Impact Sensing IoT Sensors
Integrating wireless MEMS accelerometer sensors directly onto lower upright columns provides real-time impact alerts during forklift maneuvers. Facility managers receive instant notifications of structural frame compromise, enabling preventative maintenance before structural failure occurs.
Manufacturing Benchmark
ApexDrive Enterprise Engineering Superiority & Quality Assurance
ApexDrive Industrial Racking Co., Ltd. has established itself as an authoritative manufacturer and global exporter of high-precision warehouse racking. Our manufacturing infrastructure is engineered to control quality from raw steel coils to loaded ocean shipping containers.
Traceable Raw Steel Sourcing (Q235B / Q355B)
ApexDrive utilizes prime structural steel coils exclusively supplied by Tier-1 Chinese steel mills, including Baosteel, Masteel, and Wuhan Iron and Steel. Every batch of coil comes with original Mill Test Certificates (MTC) verifying yield strength, tensile strength, and chemical composition compliance.
12M Continuous Roll Forming & ±2mm Pitch Tolerance
Equipped with 150+ sets of specialized roll-forming machinery, ApexDrive manufactures continuous upright frames up to 12 meters in a single piece without splicing welds. Automated CNC punching dies maintain a cumulative pitch tolerance under ±2 mm over 12 meters, ensuring perfect beam level alignment.
Robotic Welding & 220-Meter Swiss Gema Coating Line
Beam connectors are welded to box beams using automatic robotic manipulators, eliminating human weld porosity and missed joints. Surfaces undergo a 10-stage degreasing and rust-removal process before entering a 220-meter automated Swiss Gema electrostatic powder coating line for 180°C thermal curing.
Closed-Loop 8-Step Service Chain
From initial CAD layout design, 3D structural load calculations, and pre-shipment trial assembly to export bundle packaging, custom customs clearance documentation, and online or on-site installation guidance, ApexDrive manages the full project lifecycle.
Frequently Asked Questions
Engineering & Procurement FAQ for Overseas Buyers
Below are expert answers to common technical queries submitted by logistics directors, project managers, and industrial equipment importers when specifying VNA pallet racking systems.
Q1: What specific building data is required for ApexDrive engineers to produce a free VNA CAD layout?
To generate an accurate VNA layout and structural load design, our engineering team requires: (1) Building architectural CAD drawings detailing clear height beneath trusses, column grid spacing, building expansion joints, door locations, and sprinkler main elevation; (2) Pallet dimensions (Length × Width × Height including cargo overload) and maximum unit load weight; (3) Required total pallet capacity and SKU counts; (4) VNA forklift model, mast collapsed height, max lift height, and chassis width; and (5) Ambient operating temperature (standard room temperature vs. cold storage).
Q2: How does VNA racking compare against Radio Shuttle Racking in terms of operational cost and density?
VNA Pallet Racking provides 100% direct selectivity to every single pallet position, making it ideal for facilities with thousands of distinct SKUs and medium-to-high turnover. Radio Shuttle Racking provides higher volumetric density by storing pallets deep inside continuous lanes (LIFO or FIFO), but sacrifices 100% direct selectivity (best suited for fewer SKUs with large batch volumes). VNA initial racking equipment cost per pallet position is generally lower, but requires specialized higher-cost VNA turret trucks.
Q3: What steel grades and surface protection treatments are available for humid or cold storage applications?
For standard ambient warehouses, structural components are roll-formed from Q235B and high-strength Q355B steel, finished with a 60–80 micron electrostatic epoxy-polyester powder coating cured at 180°C. For sub-zero cold storage facilities (-25°C to -30°C) or highly humid corrosive environments, ApexDrive supplies Hot-Dip Galvanized (HDG) steel components treated according to ISO 1461 standards, preventing zinc flaking, embrittlement, and oxidation.
Q4: What floor flatness standards must be met before installing a high-bay VNA racking system?
VNA systems exceeding 10 meters in height require concrete floor slabs conforming to VDMA 23807, DIN 15185, or EN 15620 (Class 300 / 400 Superflat standards). Floor levelling measurements are taken across the narrow truck travel paths. If the existing concrete slab exceeds differential elevation tolerances, 3D laser floor grinding or steel shim leveling plates beneath upright baseplates are mandatory to prevent mast oscillation.
Q5: How are ApexDrive racking systems bundled and secured for long-distance export container transport?
All export racking bundles are packed to prevent transit abrasion and optimize container unloading space. Heavy upright frames and horizontal box beams are bundled with multi-tier high-tension steel strapping, wooden dunnage corner protectors, and heavy plastic wrap. Small hardware accessories, beam safety locks, baseplates, and anchor bolts are packed in heavy-duty corrugated cartons secured on fumigated plywood pallets.
Q6: Does ApexDrive provide on-site overseas installation support or online assembly guidance?
Yes. Every order is delivered with comprehensive 3D CAD assembly drawings, detailed step-by-step English installation manuals, and component marking lists. Our engineering team offers 24/7 remote video support. For large-scale industrial projects, ApexDrive can dispatch experienced installation supervisors and mechanical assembly crews directly to the client's site worldwide.
Ready to Optimize Your Warehouse Spatial Density?
Contact ApexDrive racking engineers today for a complimentary CAD warehouse design, structural load calculation, and factory-direct price quotation.